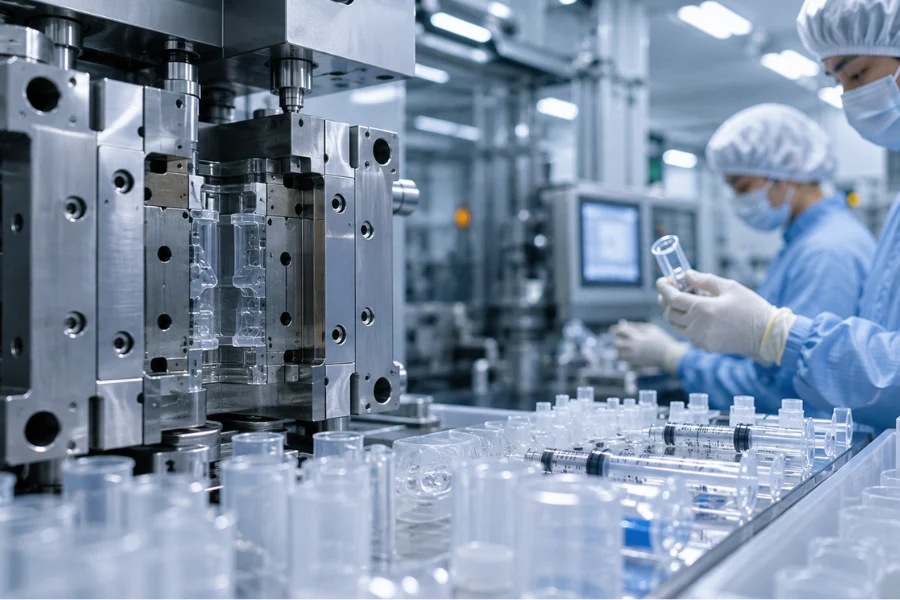
The manufacturing process of plastic products can involve molding, extrusion, forming, machining, or additive manufacturing, depending on the material, part geometry, production volume, and quality requirements.
Common plastic manufacturing processes include injection molding, extrusion, blow molding, rotational molding, thermoforming, compression molding, CNC machining, and 3D printing. Each creates parts differently, so process selection should start with the finished part requirements rather than a preferred manufacturing method.
How Are Plastic Products Manufactured?
Plastic products typically move from part and material requirements through process selection, forming, secondary operations, and inspection. The exact production sequence varies by manufacturing method.
1. Define Part and Material Requirements
Part geometry, wall thickness, dimensions, mechanical loads, operating temperature, chemical exposure, appearance, and tolerances establish the manufacturing requirements.
Material selection happens alongside these decisions. The polymer must provide the required performance while remaining compatible with the intended forming or machining process. For applications where resin properties directly affect manufacturability and performance, structured plastic material selection helps connect material requirements with the intended production method.
2. Select the Manufacturing Process
Geometry and production quantity quickly narrow the options.
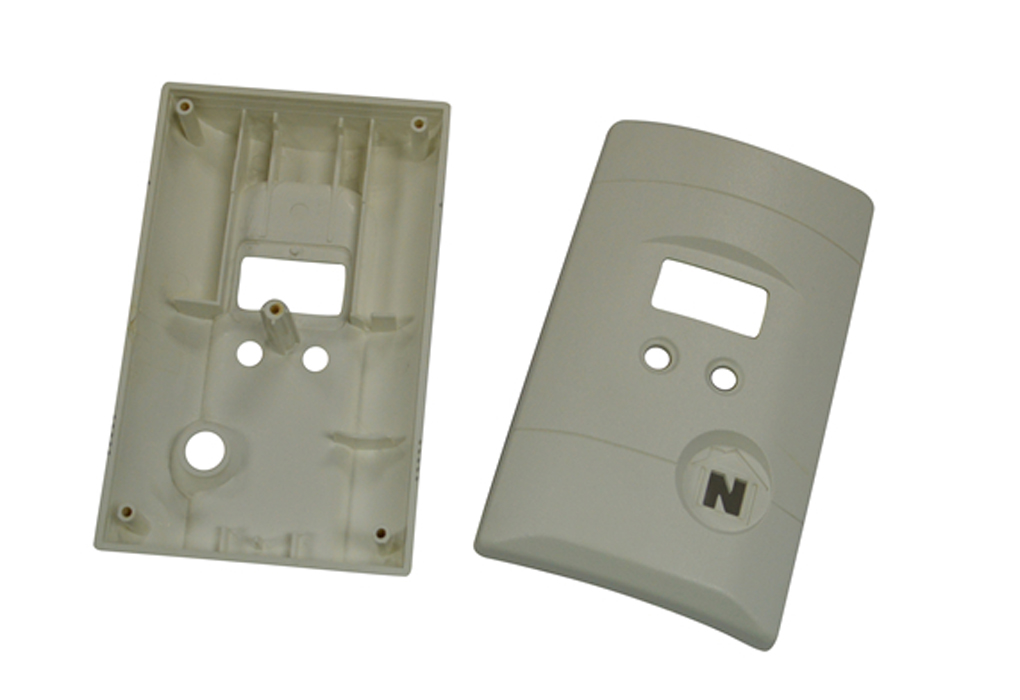
Injection molding suits many complex discrete parts produced repeatedly. Extrusion favors continuous profiles, blow molding creates hollow products, and CNC machining or 3D printing can be practical when production volumes do not justify dedicated tooling.
3. Design Tooling or the Production Setup
Mold-based processes require tooling designed around material flow, cooling, dimensional behavior, and part release. Effective mold making therefore depends on both part geometry and the processing behavior of the selected material.
Extrusion relies on a die and downstream sizing equipment, while CNC machining and many additive processes avoid dedicated production molds. Tooling decisions affect initial investment, lead time, repeatability, and eventual unit economics.
4. Form the Plastic Part
The material is shaped using heat, pressure, mechanical cutting, or layer-by-layer deposition, depending on the process.
Temperature, pressure, flow behavior, cooling rate, and processing time can influence dimensions, internal stress, surface condition, and other finished-part properties.
5. Finish and Assemble
Plastic parts may require trimming, machining, printing, coating, welding, joining, or assembly after primary manufacturing. These secondary operations should be considered during process selection because they can materially change total production cost and lead time.
6. Inspect the Parts
Inspection verifies dimensional, visual, functional, and other specified requirements. Depending on the application, production may include incoming material controls, in-process checks, dimensional inspection, functional testing, and documented quality records.
The primary forming step changes with the selected process, but material preparation, process control, finishing, and inspection remain important across many plastic parts production workflows.
Plastic Manufacturing Processes at a Glance

The major manufacturing processes for plastics differ in how material is shaped, what geometries they support, and how tooling costs scale with production volume.
| Process | Best Suited For | Production Fit | Tooling | Main Limitation |
|---|---|---|---|---|
| Injection molding | Complex discrete parts | Medium to high volume | High | Initial mold investment |
| Extrusion | Tubes, profiles, sheet and film | Continuous/high volume | Moderate | Primarily constant cross-sections |
| Blow molding | Bottles and hollow containers | Medium to high volume | Moderate to high | Mainly hollow geometry |
| Rotational molding | Large hollow products | Low to medium volume | Moderate | Longer cycles |
| Thermoforming | Trays, covers and thin shells | Low to high volume | Low to moderate | Sheet-based geometry and trimming |
| Compression molding | Thermosets and composites | Medium to high volume | Moderate | Cure time and geometry constraints |
| Transfer molding | Detailed thermoset parts and inserts | Medium volume | Moderate to high | More complex tooling and material waste |
| CNC machining | Precision parts and prototypes | Low volume | No production mold | Unit cost and material waste |
| 3D printing | Prototypes and complex low-volume parts | Low volume | No production mold | Throughput and material limitations |
These ranges are not fixed. Part size, material, tolerances, equipment, tooling strategy, and production economics can shift the practical range of each process.
Main Plastic Manufacturing Processes
Injection Molding
Plastic injection molding is widely used for the manufacturing of plastic parts when complex geometry, repeatability, and scalable production are required.
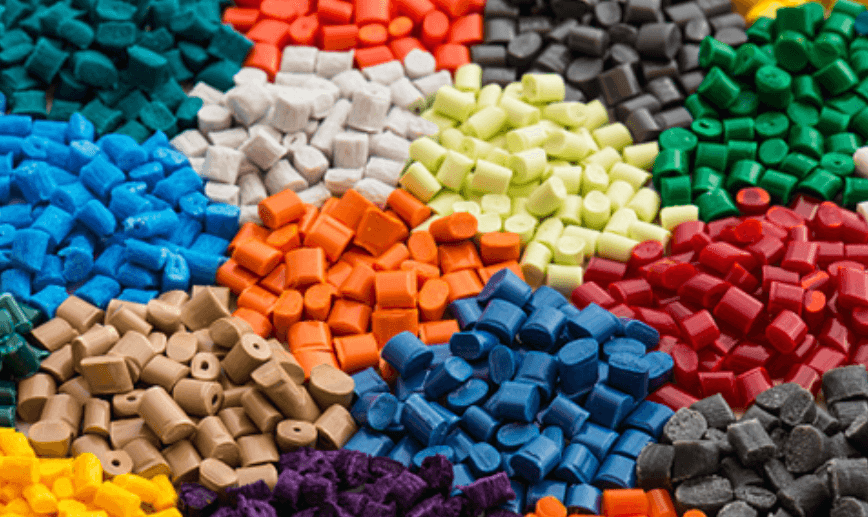
Plastic resin enters the machine through a hopper and is heated in the barrel. In a screw injection molding machine, screw rotation transports, mixes, and plasticizes the material before the screw moves forward and forces the melt into a closed mold cavity.
The molding cycle includes several connected stages:
- Plasticization: Solid resin is heated and mixed into a sufficiently uniform melt.
- Filling: Melt enters and fills the mold cavity.
- Packing and holding: Additional material compensates for volumetric contraction as the plastic begins to cool.
- Cooling: The molded part loses enough heat to become sufficiently stable for removal.
- Ejection: The mold opens and the part is released.
These stages explain why injection molding quality depends on more than simply filling the cavity. Insufficient packing can contribute to sinks, voids, shrinkage, or dimensional variation, while inappropriate melt or mold temperatures can affect filling behavior, cooling, surface condition, and cycle time.
Injection molding requires greater initial tooling investment than machining or many additive processes. Once a stable mold and process are established, however, short cycles and repeatable production can reduce unit costs at larger quantities.
Extrusion
Extrusion continuously produces plastic profiles such as tubing, sheet, film, and other products with a substantially constant cross-section.
Material moves through a rotating screw while external heating, shear, and friction help produce a uniform melt. The screw forces that melt through a shaped die, after which the extrudate is sized, cooled, pulled, and cut or wound.
Downstream control is an essential part of the process because hot thermoplastic remains deformable after leaving the die. Cooling and pulling conditions therefore influence dimensional consistency, while the die determines the basic cross-sectional geometry.
This combination makes extrusion efficient for continuous production but unsuitable when substantial three-dimensional variation is required along the length of an individual part.
Blow Molding
The defining advantage of blow molding is its ability to create enclosed hollow products such as bottles, containers, reservoirs, and ducts.
A heated preform or tube-like parison is enclosed by a mold and expanded with pressurized air until the plastic conforms to the cavity. Because the material stretches during this step, wall-thickness distribution becomes an important design and process consideration.
Blow molding is therefore selected primarily around hollow geometry rather than as a general substitute for injection molding.
Rotational Molding
Large seamless hollow parts present a different manufacturing problem. Rotational molding addresses it by distributing polymer over the internal surfaces of a hollow mold rather than forcing melt into the cavity at high pressure.
The mold is heated while rotating around multiple axes, allowing the material to progressively distribute and fuse before cooling. Tanks, bins, housings, and recreational products are common examples.
Relatively low molding pressure can simplify certain tooling requirements, but the heating and cooling cycle is comparatively long, limiting production rate.
Thermoforming and Vacuum Forming
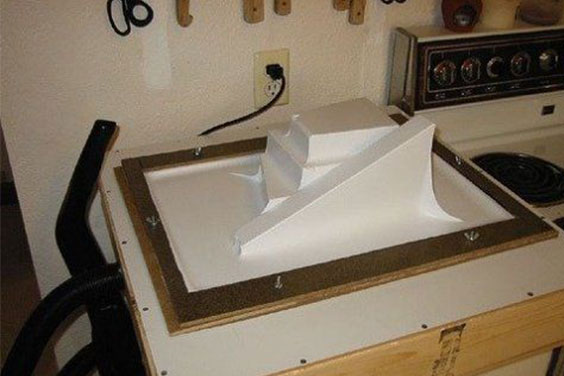
Thermoforming starts with a thermoplastic sheet instead of filling a cavity with molten resin. The sheet is heated until formable, shaped over or into a mold, cooled, and then trimmed.
Vacuum forming is a thermoforming method that uses vacuum pressure to draw the softened sheet against the mold surface.
This approach works well for trays, packaging, covers, liners, and other shell-like products. Tooling can be simpler than injection molds, although sheet stretching, wall thinning, trimming requirements, and the limitations of sheet-based geometry must be considered during design.
Compression Molding
For thermosetting plastics and certain composite materials, manufacturing involves curing as well as shaping. Compression molding performs both operations inside a heated mold.
A measured material charge is placed into the open mold before it closes and applies pressure. The material flows through the cavity while heat promotes curing and cross-linking.
A typical sequence is:
material preparation → loading → mold closing → venting when required → curing → demolding
Temperature, pressure, and curing time must work together. Insufficient curing can compromise part properties, while unnecessary cure time reduces productivity. Excessive molding pressure also increases loads on the tooling.
Transfer Molding
Transfer molding also commonly processes thermosetting materials, but material is forced from a transfer chamber into an already closed mold rather than being loaded directly into the open cavity.
This arrangement can support detailed features, thin sections, and molded-in inserts. The trade-offs are more complex tooling and additional material in the transfer and runner system.
CNC Machining
CNC plastic machining approaches plastic part production differently because the geometry is cut from existing plastic stock rather than formed in a mold.
Computer-controlled cutting tools remove material from sheet, rod, or block. The absence of dedicated molding tooling makes machining useful for prototypes, low-volume components, and many precision engineering parts.
Material waste and machining time remain in each production cycle, however, so unit economics can become less favorable as quantities increase.
3D Printing
3D prototype printing builds plastic parts directly from digital geometry, layer by layer, without a conventional production mold.
This makes additive manufacturing useful for prototypes, design iterations, fixtures, and complex low-volume components. Certain geometries can also be produced without the tool-access or mold-release constraints associated with machining and molding.
The practical limits depend on the printing process and can include throughput, material selection, surface finish, dimensional behavior, and direction-dependent mechanical properties. 3D printing should therefore be evaluated against the actual part requirements rather than treated as a universal replacement for molded production.
Materials Used in Plastic Manufacturing
Material and process selection should be considered together. Melt behavior, thermal stability, shrinkage, crystallization, moisture sensitivity, reinforcement, and other material characteristics can determine whether a plastic manufacturing process is practical and how tightly it can be controlled.
| Material | Relevant Characteristics | Common Processes | Processing Considerations |
|---|---|---|---|
| Polyethylene (PE) | Tough, chemically resistant, available in multiple densities | Extrusion, blow molding, injection molding | Grade and density affect shrinkage, stiffness and processing behavior |
| Polypropylene (PP) | Low density, chemical resistance, fatigue resistance | PP injection molding, extrusion, thermoforming | Semi-crystalline behavior influences shrinkage and dimensional control |
| Polyvinyl chloride (PVC) | Available in rigid and flexible formulations | Extrusion, injection molding | Processing temperature requires control because of limited thermal stability |
| PET | Strength, chemical resistance and useful barrier properties | Blow molding, PET injection molding, extrusion | Moisture control before melt processing is important |
| PETG | Clear and readily thermoformable depending on grade | Thermoforming, extrusion, injection molding | Processing and drying conditions should follow the selected grade and process |
| ABS | Impact resistant and readily processable | ABS plastic molding, extrusion, CNC machining | Moisture and thermal conditions can affect molded quality |
| Polycarbonate (PC) | High impact resistance and available in transparent grades | Injection molding, extrusion, CNC machining | Moisture control and relatively high processing temperatures are typically required |
Material grade matters as much as polymer family. Fillers, glass reinforcement, additives, molecular characteristics, and regulatory requirements can change melt flow, shrinkage, processing temperature, tooling wear, and finished-part performance.

How to Choose the Right Plastic Manufacturing Process
There is no single best method for plastic parts production. Process selection depends on how geometry, material behavior, production quantity, quality requirements, and manufacturing economics interact.
Part Geometry
Geometry can eliminate unsuitable processes before detailed cost comparisons begin.
Continuous constant-section products naturally favor extrusion, while hollow containers may favor blow molding. Large hollow parts can suit rotational molding, and geometrically complex discrete components are often candidates for injection molding.
Machining and 3D printing become particularly useful when geometry or production quantity does not justify dedicated tooling.
Material Requirements
Thermoplastics can generally be reheated and reshaped, while thermosetting materials undergo irreversible curing. Within those groups, melt viscosity, thermal stability, crystallization, reinforcement, and moisture sensitivity further affect process compatibility.
Material requirements therefore need to be evaluated at the grade level, not only by polymer family.
Production Volume
Production quantity changes the economics of the same part.
Injection molding requires mold investment but can provide short cycles and repeatable production after tooling is established. CNC machining and 3D printing avoid production molds but usually retain more manufacturing time and cost in each additional part.
Tolerance and Quality Requirements
Every manufacturing process introduces different sources of dimensional variation.
Molding may be affected by shrinkage, cooling, warpage, tooling, and process stability. Machining depends more directly on material stability, cutting conditions, workholding, and machine capability.
Tight requirements can therefore influence the process, tooling, inspection strategy, and even the part design.
Tooling, Cost, and Lead Time
The lowest tooling price does not necessarily produce the lowest finished-part cost.
Tooling, material utilization, machine time, labor, secondary operations, inspection, expected quantity, and tool life all contribute to total manufacturing economics. Mold-based processes also require tooling design, fabrication, trials, and qualification before production, whereas machining and additive manufacturing can often produce initial parts sooner.
For molded components, early mold tool design can help identify tooling constraints before they become more expensive to address during mold fabrication or production.
Secondary Operations
Trimming, machining, welding, printing, coating, assembly, and inspection can materially change the economics of the primary manufacturing process.
A method with inexpensive forming may not provide the lowest finished-part cost if extensive secondary work is required.
Plastic Manufacturing for Medical Parts
Medical plastic parts use the same underlying manufacturing principles as other engineered components, but additional controls may apply depending on the device, material, production stage, and regulatory requirements.
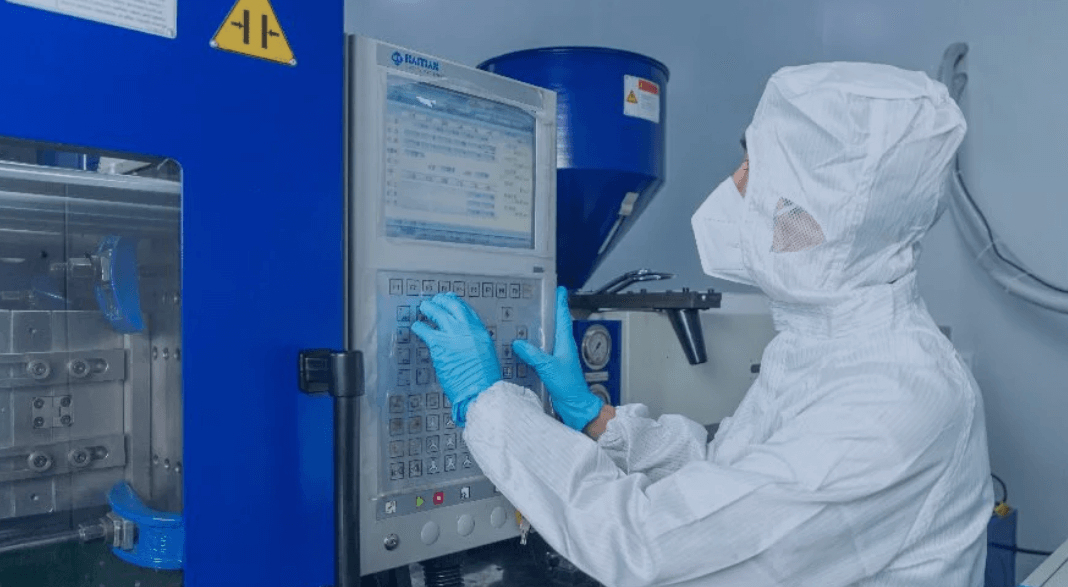
These may include material traceability, controlled manufacturing conditions, documented process parameters, inspection, validation, assembly controls, and contamination management. Cleanroom injection molding is appropriate when product and manufacturing requirements call for controlled particulate or contamination conditions; it is not a universal requirement for every plastic component.
For injection-molded medical components, DFM should also consider resin behavior, wall thickness, filling, cooling, shrinkage, part release, tooling, and the ability to maintain a repeatable process. SeaSkyMedical supports medical plastic injection molding, tooling, medical device assembly, and medical device verification and validation where these capabilities are required.
Frequently Asked Questions
What Is the Difference Between Injection Molding and Extrusion?
Injection molding fills a closed mold cavity to produce individual parts with three-dimensional geometry. Extrusion continuously forces plastic through a die and is primarily used for products with a substantially constant cross-section.
Which Plastic Manufacturing Process Is Suitable for Low-Volume Parts?
CNC machining and 3D printing are often practical for low-volume parts because they avoid dedicated production molds. Low-volume injection molding or thermoforming may also be viable when expected future volume, geometry, material, and tooling economics justify the setup.
How Does Production Volume Affect Plastic Manufacturing Cost?
Processes requiring dedicated tooling usually have higher initial costs but can distribute that investment across larger production quantities. Tool-free processes such as CNC machining and 3D printing reduce upfront investment but often retain higher incremental manufacturing costs per part.
Conclusion
No single plastic manufacturing process fits every product. The appropriate method depends on how material behavior, geometry, quality requirements, production quantity, and manufacturing economics interact.
For medical plastic components that require controlled molding, tooling, assembly, or validation support, SeaSkyMedical can help evaluate the manufacturing approach and develop a process suitable for scalable production.