Plastic molding is a family of manufacturing processes that shape polymer materials using molds, dies, heat, pressure, air, vacuum, or rotational motion. Major methods include injection molding, blow molding, compression molding, extrusion, rotational molding, thermoforming, and transfer molding.
Each method suits different part geometries, materials, production volumes, and quality requirements. This guide explains how these processes work, where they differ, and how to choose between them.
What Is Plastic Molding?
In custom plastic molding, polymer material is shaped into a defined geometry according to specific part, material, and production requirements. A mold is the tooling that defines some or all of the part geometry, while molding refers to the process used to form the material.
The shaping mechanism varies. Injection molding pushes molten polymer into a closed cavity, compression molding presses material within heated tooling, blow molding expands heated plastic with air, and rotational molding distributes material over the inside of a rotating mold.
Part quality depends on more than mold geometry. Material behavior, tooling design, equipment, temperature, pressure, cooling or curing, and process consistency can affect dimensions, surface quality, internal stress, and repeatability.
How Does the Plastic Molding Process Work?
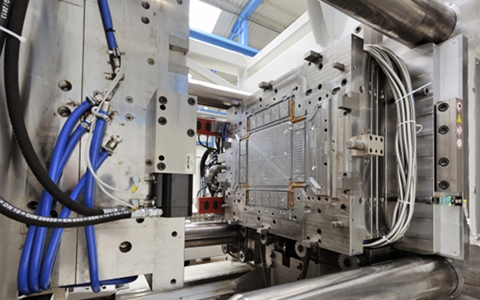
There is no universal cycle for every method, but most involve several common stages:
- Material preparation: Resin, pellets, powder, sheet, or molding compound is selected and prepared. Moisture-sensitive materials may require drying.
- Heating or conditioning: The material is melted, softened, or prepared for forming. Thermosets may instead rely on heat to initiate curing.
- Shaping: Material is injected, compressed, blown, extruded, rotated, or otherwise formed against tooling.
- Cooling or curing: Thermoplastics generally solidify as they cool, while thermosets cure through chemical cross-linking.
- Part removal and finishing: The part is removed and may require trimming, machining, conditioning, assembly, or other secondary operations.
The exact sequence depends on the process. Injection molding, for example, includes plasticizing, cavity filling, packing or holding, cooling, and ejection.
Main Types of Plastic Molding Processes
The major plastic molding techniques solve different manufacturing problems. Their most important differences involve how the material is shaped and what geometry that mechanism can produce efficiently.
Injection Molding
Injection molding plasticizes polymer material in a heated barrel and uses a screw to drive the melt through a nozzle and runner/gate system into a closed mold cavity.
Pressure is maintained after filling to compensate for material contraction as the part cools. Once sufficiently rigid, the mold opens and the part is ejected.
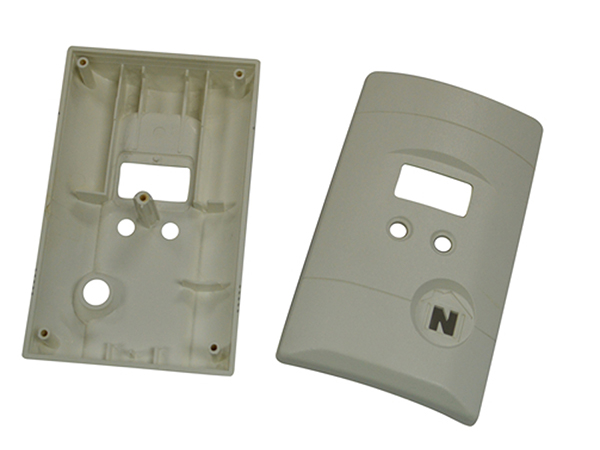
The method is well suited to repeat production of detailed three-dimensional components such as medical device parts, housings, connectors, gears, caps, and automotive components.
Key advantages
- Complex three-dimensional features
- Good repeatability with appropriate tooling and process control
- Efficient medium- and high-volume production
- Broad thermoplastic material selection
- Insert molding capability
Key limitations
- Significant upfront tooling investment
- Costly design changes after tooling is completed
- DFM constraints involving wall thickness, draft, gates, cooling, shrinkage, and ejection
- Less attractive economics for very small production quantities
Because mold architecture affects filling, cooling, ejection, and repeatability, mold manufacturing should be evaluated together with part design and production requirements.
Cycle time varies with material, part size and thickness, mold configuration, machine capability, and process conditions rather than following a universal value.
Blow Molding
Blow molding produces hollow plastic parts by enclosing a heated parison or preform within a mold and using pressurized air to expand it against the cavity walls. The formed part is cooled before removal.
This process is commonly used for bottles, reservoirs, fluid containers, and other hollow products. Extrusion blow molding, injection blow molding, and stretch blow molding differ in how the starting material is prepared and formed.
Blow molding is efficient for enclosed hollow geometries, but material stretching makes wall-thickness distribution an important process consideration. The method is generally less suitable for detailed solid components.
Compression Molding
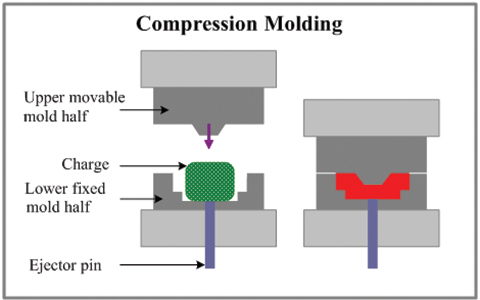
Compression molding places a measured charge of material into an open, heated mold. The mold closes and applies pressure, causing the material to flow through the cavity before curing or solidifying.
The process is strongly associated with thermosetting materials and composites. Conventional thermoset compression molding can involve loading, mold closing, venting, curing, and part removal.
It is commonly considered for relatively large, thick, or structural components, including electrical and automotive applications. Compression molding can use relatively direct tooling and accommodate many thermosets and composites, although fine features, flash control, and curing requirements can complicate production.
Pressure, mold temperature, and cure time interact. Excessive pressure can increase tooling loads, while inappropriate temperature or cure time can contribute to incomplete filling, internal stress, deformation, or reduced material performance.
Extrusion Molding
Extrusion continuously feeds polymer into an extruder, where heat and screw action plasticize and transport the material before forcing it through a shaped die.
The material exits with a continuous cross-sectional profile and is then sized where necessary, cooled, pulled forward, and cut to length or wound.
Common products include pipes, tubing, seals, weatherstripping, construction profiles, sheet, film, and wire insulation.
Extrusion provides high-output production for continuous products, but that advantage also defines its geometric limitation: it is intended for profiles with a substantially consistent cross section rather than arbitrary three-dimensional parts.
Temperature, screw speed, pressure, and haul-off speed must remain sufficiently stable because fluctuations can affect dimensions and product quality.
Rotational Molding
Rotational molding, or rotomolding, is primarily used for large hollow components. A measured quantity of polymer is placed inside a hollow mold, which is heated while rotating around multiple axes.
As the material melts, rotation distributes it across the internal mold surfaces. The mold then cools before the solidified part is removed.
Rotomolding works well for tanks, bins, containers, recreational products, and other hollow parts that would be difficult or uneconomical to manufacture with high-pressure molding. Comparatively economical tooling can be an advantage, while longer cycles, lower throughput, and more limited dimensional precision restrict its use for many high-volume precision components.
Thermoforming
Thermoforming starts with thermoplastic sheet. The sheet is heated until formable and shaped over or into tooling using vacuum, pressure, mechanical force, or a combination of these methods.
After cooling, the part is normally trimmed from the surrounding sheet. Typical applications include trays, covers, liners, packaging, equipment panels, and large thin-walled shells.
Tooling can be relatively straightforward for suitable parts. However, sheet stretching can produce wall-thickness variation, trimming adds another manufacturing step, and detailed precision features can be more difficult to control than with injection molding.
Transfer Molding
Transfer molding is closely related to compression molding and is primarily associated with thermosetting materials. The molding compound is heated in a transfer chamber and forced through a runner and gate system into a closed cavity.
Because the material flows before entering the cavity, transfer molding can accommodate intricate geometries, thinner sections, and inserts that may be more difficult to produce by conventional compression molding. Trade-offs include more complex tooling and material loss through the transfer and runner system.
It is commonly used for electrical components, encapsulation, connectors, and other thermoset parts incorporating inserts.
Plastic Molding Processes Compared
The main differences between these processes become clearer when they are compared by shaping mechanism and suitable part geometry.
| Process | Shaping Principle | Best-Suited Geometry | Typical Material Form | Common Production Use | Main Limitation |
|---|---|---|---|---|---|
| Injection molding | Melt injected into closed cavity | Detailed 3D parts | Mainly thermoplastic pellets | Repeat medium- to high-volume parts | Higher tooling investment |
| Blow molding | Air expands heated polymer | Hollow containers | Parison or preform | Bottles, containers, and reservoirs | Limited solid geometry |
| Compression molding | Material pressed in heated mold | Thick or structural parts | Thermoset/composite charge | Structural and thermoset components | Longer cycles in many applications |
| Extrusion | Melt forced through die | Continuous profiles | Mainly thermoplastic resin | Tubing, profiles, sheet, and film | Substantially constant cross section |
| Rotational molding | Heated mold rotates material | Large hollow parts | Typically polymer powder | Tanks, bins, and large hollow products | Long cycle time |
| Thermoforming | Heated sheet formed over tooling | Thin shells and panels | Thermoplastic sheet | Packaging, trays, panels, and large shells | Wall-thickness variation |
| Transfer molding | Material transferred into closed cavity | Detailed thermoset parts and inserts | Thermoset compound | Insert and encapsulation applications | More complex tooling |
These are general tendencies rather than fixed process limits. Resin behavior, part dimensions, tolerance, tooling architecture, equipment, expected volume, and quality requirements can change the practical choice.
How to Choose the Right Plastic Molding Process
Process selection should start with the physical requirements of the part. Tooling price becomes meaningful only after unsuitable manufacturing methods have been eliminated.
Use Geometry to Narrow the Options
Geometry is often the fastest filter. Detailed three-dimensional parts commonly favor injection molding, while hollow or continuous geometries require fundamentally different shaping mechanisms.
The objective is to identify which process can create the required shape efficiently and repeatably before comparing tooling and production costs.
Match the Process to Material Behavior
Material selection can narrow the practical molding options because polymers respond differently to heat, pressure, cooling, and curing.
Thermoplastics soften when heated and can generally be remelted, supporting processes such as injection molding and extrusion. Thermosets cure through chemical reactions and cannot simply be remelted after curing, making compression and transfer molding important alternatives for many applications.
Melt viscosity, thermal stability, moisture sensitivity, crystallization, shrinkage, and reinforcement can further narrow the practical process window.
Evaluate Volume and Tooling Economics Together
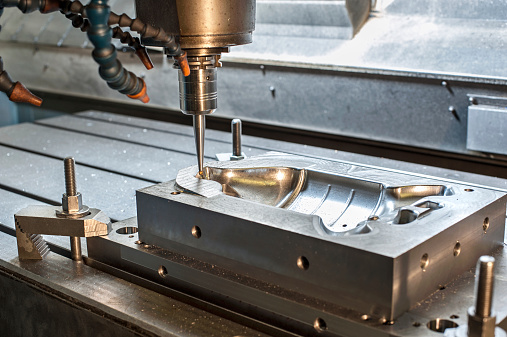
Production volume changes how tooling cost should be evaluated.
Injection molding may justify substantial mold investment when that cost can be distributed across repeat production. A lower-volume, very large, or geometrically simpler part may favor a process with different tooling and equipment requirements.
Expected lifetime demand is therefore more useful than comparing mold quotations alone.
Define Quality Requirements Before Tooling
Tolerance, surface requirements, critical dimensions, and repeatability should be defined before selecting the final process and tooling concept.
Material shrinkage, cooling uniformity, mold temperature, forming behavior, trimming, and process variation affect different methods in different ways. A process capable of producing the basic shape may still be unsuitable if it cannot economically maintain the required quality.
Check Wall Structure and Part Size
Part dimensions influence flow, cooling, forming behavior, and cycle time.
In injection molding, thin sections increase flow resistance and cool quickly, while thick sections require more cooling and can increase shrinkage-related concerns.
Process selection should therefore consider not only overall shape but also how material must move, cool, or cure throughout the part.
Other Specialized Plastic Forming Methods
Plastic manufacturing also includes casting, laminating, FRP and composite processes, and other specialized forming technologies. These may produce polymer-based components, but they differ from the primary molding methods in starting material, tooling, curing mechanism, and production economics.
They are better evaluated for specific material and product requirements rather than treated as equivalent alternatives to injection, blow, compression, extrusion, rotational, thermoforming, or transfer molding.
Plastic Molding for Medical Device Manufacturing
Medical plastic components may introduce requirements beyond basic process selection. Medical plastic injection molding projects can require closer consideration of material compatibility, dimensional requirements, contamination control, tooling strategy, process consistency, assembly, packaging, and validation needs.
For an injection-molded medical component, DFM should address wall thickness, draft, gates, parting lines, ejection, shrinkage, cooling, and critical dimensions before tooling is finalized. Early mold and tooling design can help identify these manufacturability constraints before production tooling is completed.
Depending on the device and contamination-control requirements, production may also require cleanroom injection molding rather than conventional molding conditions. Material handling and molding conditions then need to remain controlled throughout production.
Medical manufacturing requirements can extend beyond molding itself. Where applicable, medical device verification and validation should be considered alongside manufacturing, quality, and product requirements.
SeaSkyMedical supports medical injection molding projects from DFM and mold manufacturing through cleanroom molding, validation support, assembly, and packaging. The manufacturing route should still be selected according to the product requirements rather than assuming injection molding is appropriate for every medical plastic component.
FAQ
What Are the Main Types of Plastic Molding?
Common plastic molding processes include injection molding, blow molding, compression molding, extrusion, rotational molding, thermoforming, and transfer molding. Each uses a different shaping mechanism and suits different materials and part geometries.
Which Plastic Molding Process Is Best for High-Volume Parts?
Injection molding is commonly used for high-volume production of detailed three-dimensional parts, while extrusion provides high continuous output for constant-profile products and blow molding can efficiently produce hollow containers. The best process depends on geometry, material, volume, and quality requirements rather than volume alone.
What Is the Difference Between Injection Molding and Extrusion?
Injection molding fills a closed mold cavity to produce individual three-dimensional parts. Extrusion continuously forces plastic through a die and is better suited to products with a substantially consistent cross section, such as tubing and profiles.
Which Plastic Molding Process Is Used for Hollow Parts?
Blow molding is widely used for bottles and similar hollow containers. Rotational molding is another option, particularly for larger hollow products such as tanks and bins.
How Do You Choose a Plastic Molding Method?
Start with part geometry and material, then evaluate production volume, tolerance, surface requirements, wall structure, part size, tooling investment, and production economics. The selected process should satisfy the physical and quality requirements of the part before cost optimization begins.