Transfer molding, injection molding, and compression molding all use heat and pressure to form polymer materials, but they differ in how the material is prepared, introduced into the mold, and solidified.
The right process depends on the material system, part geometry, tooling requirements, production volume, dimensional requirements, and automation needs. For medical components, material compatibility, cleanliness, validation, and production scalability can also affect the decision.
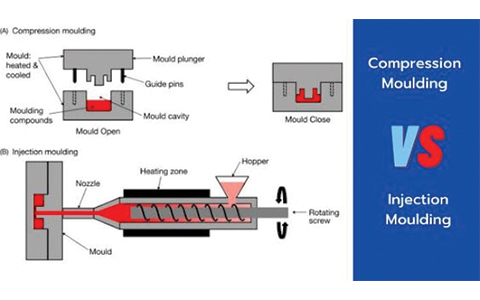
Transfer Molding vs Injection Molding vs Compression Molding: Key Differences
The simplest way to distinguish the three processes is to look at where the molding material is placed, how it reaches the cavity, and how the part develops its final properties.
| Factor | Compression Molding | Transfer Molding | Injection Molding |
|---|---|---|---|
| Initial material placement | Charge placed in mold | Charge placed in transfer pot | Material loaded into injection unit |
| Mold state during cavity filling | Mold closes around the charge | Mold is closed before transfer | Mold is closed before injection |
| Material delivery | Direct compression | Plunger, runners, and gates | Injection unit and mold filling system |
| Common material systems | Thermosets, composites, elastomers | Thermosets, elastomers, selected encapsulation systems | Mainly thermoplastics, plus suitable thermoset systems |
| Part complexity | Simple to moderately complex | Moderate to complex | Moderate to highly complex |
| Insert capability | Application dependent | Strong capability | Strong capability |
| Tooling requirements | Relatively straightforward for suitable parts | More complex than basic compression | Can become highly complex for advanced geometries |
| Automation potential | Application dependent | Medium to high | High |
| Cycle-time potential | Often longer for thermoset curing | Can be shorter than conventional compression | Often efficient for scalable production |
| Material waste | Can be relatively low | Transfer system adds material | Depends on runner, gate, and hot-runner design |
| Typical production fit | Large or suitable low-to-medium-volume parts | Complex thermoset or elastomer parts and inserts | Repeatable, scalable production |
These are general process tendencies rather than universal rules. Actual tooling cost, cycle time, material utilization, and production economics depend on material behavior, part geometry, cavity count, machine configuration, mold design, and required production volume.
A Quick Process Selection Guide
| If the project priority is… | Start by evaluating… |
|---|---|
| Large or relatively straightforward thermoset part | Compression molding |
| Complex thermoset part with inserts | Transfer molding |
| Complex thermoplastic component | Injection molding |
| Highly automated, scalable production | Injection molding |
| Controlled material flow around inserts | Transfer molding |
| Relatively straightforward tooling for a suitable geometry | Compression molding |
| Thermoset processing with injection-based material delivery | Thermoset injection molding |
These are starting points rather than universal rules. Material formulation, geometry, annual volume, tooling requirements, and quality requirements should be evaluated together.
What Is Compression Molding?
Compression molding forms a part by placing a measured material charge into a heated mold and applying pressure as the material flows and cures or solidifies inside the cavity.
It is widely associated with thermosets, composites, and elastomers. The source material describes the process as placing powder, granular, fragmented, or fibrous thermosetting material into the mold, followed by mold closing, heating, pressure application, and curing.
How Compression Molding Works
A typical compression molding cycle includes:
- Material preparation, including preheating or preforming when required.
- Placement of the material charge into the mold.
- Mold closing.
- Application of pressure and heat.
- Material flow and cavity filling.
- Curing or solidification.
- Mold opening and part removal.
- Trimming or secondary finishing when required.
For thermosetting materials, temperature affects both material flow and the rate of the crosslinking reaction. Preheating can also remove moisture and volatile components while helping reduce the molding cycle.
Compression Molding Advantages and Limitations
Compression molding can be useful when a component does not require the complex cavity-filling system associated with injection or transfer molding.
Potential advantages include:
- Relatively straightforward tooling for suitable geometries
- Compatibility with many thermoset and composite materials
- Suitability for relatively large components
- Potentially efficient material utilization when the charge is accurately controlled
- Practical production of parts that do not require highly complex flow paths
Its limitations become more important with intricate geometries, deep features, fine details, and applications requiring highly automated production. Longer curing cycles and secondary flash removal can also influence production economics.
Compression Molding Materials and Applications
Compression molding can be used with:
- Phenolic molding compounds
- Epoxy systems
- Amino resins
- Unsaturated polyester systems
- Glass-fiber-reinforced compounds
- Carbon-fiber-reinforced compounds
- Sheet molding compound (SMC)
- Bulk molding compound (BMC)
- Selected elastomers
Applications include automotive, electrical, consumer, composite, and selected medical components. The historical source also identifies syringe stoppers and respirator-related components among medical and dental applications.
For medical components, material compatibility, dimensional stability, cleanliness, and functional requirements should be evaluated alongside the molding process.
Compression Mold Types and Flash Control
Compression molds can use different approaches to manage excess material and flash.
- Open-flash molds allow excess material to escape at the parting line and can tolerate some variation in the material charge.
- Positive molds provide tighter control over the charge and part dimensions but require more accurate material measurement.
- Semi-positive molds provide an intermediate approach.
These configurations affect material utilization, flash, dimensional consistency, and secondary finishing requirements.
What Is Injection Molding?
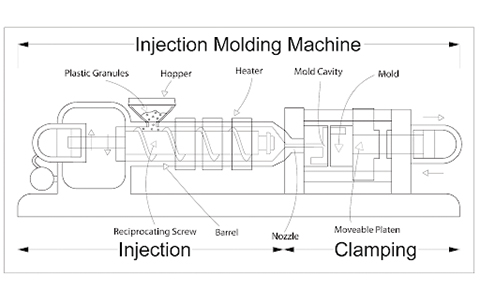
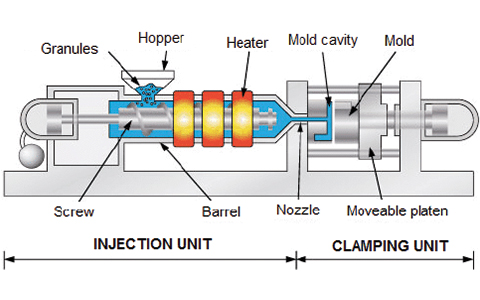
Injection molding plasticizes a material and forces it under pressure through an injection system into a closed mold cavity. The material is then cooled or cured under controlled conditions before the mold opens and the part is ejected.
The process is widely used for complex components and scalable production because material preparation, injection, packing, cooling or curing, and ejection can be integrated into a repeatable cycle.
For a broader technical explanation, see A Complete Guide to Injection Molding.
How Injection Molding Works
A typical injection molding cycle includes:
- Material preparation — molding material is prepared for processing.
- Plasticizing — the material is heated and plasticized inside the injection unit.
- Clamping — the mold halves are closed and held under sufficient clamping force.
- Injection — the plasticized material enters the closed cavity through the mold filling system.
- Packing and holding — pressure is maintained as required to compensate for material shrinkage.
- Cooling or curing — the part develops its final form and properties.
- Ejection — the mold opens and the finished part is removed.
For thermoplastic injection molding, solidification primarily occurs through cooling. Thermoset injection molding follows a different mechanism because the material undergoes chemical crosslinking and cures inside the heated mol
Injection Molding Advantages and Limitations
Injection molding can provide:
- High production output
- Repeatable part geometry
- Strong automation potential
- Multi-cavity production
- Good suitability for complex features
- Efficient unit economics at appropriate production volumes
The main trade-offs are usually associated with tooling and equipment investment. Complex injection molds may require slides, lifters, specialized cores, cooling circuits, sophisticated ejection systems, or high-cavity-count tooling.
Large parts can also be constrained by machine size, mold dimensions, clamping force, and injection capacity.
Injection Molding Materials
Many injection-molded products use thermoplastics such as:
- Polypropylene (PP)
- Polyethylene (PE)
- Polycarbonate (PC)
- Acrylonitrile butadiene styrene (ABS)
- Polyamide (PA)
- Polyoxymethylene (POM)
- PMMA
- TPU
- TPE
For medical components, material selection can also involve mechanical requirements, chemical resistance, sterilization compatibility, dimensional stability, and applicable quality or regulatory requirements.
SeaSkyMedical supports medical plastic injection molding for applications where injection molding matches the component and material requirements.
What Is Transfer Molding?
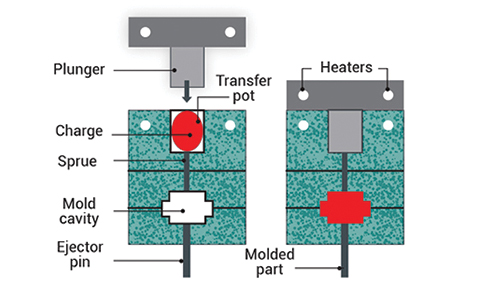
Transfer molding uses a measured molding charge placed into a separate transfer pot or chamber. After the mold is closed, a plunger applies pressure and forces the material through a transfer system into the mold cavity.
This makes transfer molding different from compression molding because the material does not simply remain in the cavity while the mold applies compression. Instead, the material is transferred through a defined flow path before entering the cavity.
Transfer molding is commonly associated with thermosets and elastomers and can be useful for parts requiring inserts, more complex features, or controlled filling of closed cavities.
How Transfer Molding Works
A simplified transfer molding process is:
- Prepare and accurately measure the molding charge.
- Place the charge into the transfer pot.
- Close the mold.
- Apply pressure through the transfer plunger.
- Force the material through runners and gates.
- Fill the closed cavities.
- Maintain heat and pressure while the material cures.
- Open the mold and remove the molded parts.
- Remove the transfer pad, sprue, or other excess material when required.
The defining process difference is therefore:
Compression molding places the charge in the mold, while transfer molding places the charge in a transfer chamber and moves it into a closed cavity.
Transfer Mold Tooling
A transfer mold typically contains more components than a basic compression mold because the material must move from the charge chamber into the closed cavity.
Important elements can include:
- Transfer pot or charge chamber
- Plunger
- Mold cavity
- Core and other molding components
- Runners
- Gates
- Heating system
- Guide and alignment components
- Ejection system
The transfer system provides controlled material movement into the cavity, but it also adds tooling complexity and can generate additional material in the transfer pad and flow system.
Transfer Molding Advantages and Limitations
Transfer molding can be useful when compression molding does not provide enough control over cavity filling or part geometry.
Potential advantages include:
- Better suitability for complex features
- Good compatibility with inserts
- Controlled material flow into closed cavities
- Ability to form relatively deep or detailed features
- Potentially shorter curing cycles than conventional compression molding for suitable materials and mold designs
- Useful processing options for thermosets and elastomers
The additional transfer system also introduces trade-offs:
- More complex tooling
- Additional material in the transfer pad, sprue, and runners
- Additional mold cleaning and maintenance
- Gate or transfer marks that may need to be considered during design
The appropriate balance depends on part geometry, material, production volume, tooling requirements, and the value gained from controlled cavity filling.
Transfer Molding Materials and Applications
Transfer molding is commonly used with thermosetting materials and elastomers. Examples can include:
- Phenolic compounds
- Epoxy systems
- Amino resins
- Selected silicone and rubber systems
- Other thermosetting molding compounds
Applications can include insert-based components, sealing parts, encapsulation-related applications, electrical components, and other parts where controlled material transfer is useful.
Transfer Molding vs Compression Molding
Transfer molding and compression molding are closely related, particularly for thermosetting materials, but the material delivery mechanism is fundamentally different.
Compression Molding
In compression molding, the material charge is placed directly into the mold area. The mold then applies heat and pressure to distribute the material and complete curing or solidification.
This approach can simplify the tooling and material delivery system for suitable geometries.
Transfer Molding
In transfer molding, the material is placed in a transfer pot and forced through runners and gates into a closed cavity by a plunger.
This additional flow path can provide better control for parts with inserts, deeper features, or more complex geometry.
| Consideration | Compression Molding | Transfer Molding |
|---|---|---|
| Charge location | Mold cavity or charge area | Transfer pot |
| Mold condition | Closes around charge | Closed before transfer |
| Cavity filling | Direct compression | Pressure-driven transfer |
| Tooling | Generally simpler | More complex |
| Inserts | Application dependent | Particularly suitable |
| Complex features | More limited | Generally more capable |
| Material waste | Potentially lower | Higher due to transfer system |
| Process control | Relatively straightforward | Greater control of material transfer |
The additional tooling of transfer molding is most useful when controlled cavity filling, inserts, or geometry justify the added complexity.
Injection Molding vs Compression Molding
The main distinction between injection molding and compression molding is the way the material reaches the cavity and how that affects production strategy.
Injection molding plasticizes and injects material into a closed cavity. Compression molding places a material charge into the mold and uses heat and mechanical pressure to form and cure or solidify the part.
Injection molding is often considered when:
- The part has complex geometry.
- Repeatability is important.
- Production volume can justify injection tooling.
- Automated production is desirable.
- Multiple cavities can improve production economics.
- The material has suitable injection-processing characteristics.
Compression molding can be considered when:
- The material is well suited to compression processing.
- The component is relatively large or less geometrically complex.
- Simpler tooling is sufficient.
- Thermoset, composite, or elastomer processing is required.
- The required production rate can accommodate the molding cycle.
The choice is therefore not simply “injection versus compression.” Material, geometry, tooling, production volume, and process requirements all influence the decision.
Transfer Molding vs Injection Molding
Transfer molding and injection molding both use pressure-driven material flow into a closed mold, but their material delivery systems are different.
Transfer molding uses a separate charge chamber and plunger to push material through a transfer system into the cavity. Injection molding uses an injection unit to plasticize, meter, and inject the material through the nozzle and mold filling system.
The most important comparison points are therefore:
- Material system — transfer molding is commonly associated with thermosets and elastomers, while conventional injection molding is widely used for thermoplastics.
- Material delivery — transfer molding uses a transfer pot and plunger; injection molding uses an injection unit.
- Tooling — transfer tooling adds the transfer system, while injection tooling can become highly complex when the part requires multiple cavities, slides, lifters, or specialized cooling.
- Production strategy — injection molding can provide strong automation and scalability, while transfer molding can be advantageous when controlled thermoset or elastomer processing and inserts are important.
Neither process should be selected solely because one has a lower machine or mold cost. The complete manufacturing system should be evaluated.
How Material Choice Affects Process Selection
Material behavior is one of the first variables to evaluate because thermoplastics and thermosets respond differently to heat and pressure.
Thermoplastics
Thermoplastics can be softened by heating and solidified again by cooling. Many thermoplastics are therefore well suited to injection molding.
Representative materials include PP, PE, PC, ABS, PA, POM, TPU, and TPE.
Thermosets
Thermosetting materials undergo an irreversible chemical crosslinking reaction during curing. Phenolic compounds, epoxy systems, amino resins, and selected polyester systems can be processed through compression or transfer molding depending on the formulation and part requirements.
Thermoset Injection Molding
Suitable thermosetting compounds can also be injection molded.
The important distinction is what happens after injection. With conventional thermoplastic injection molding, the material generally solidifies through cooling. With thermoset injection molding, the material cures through crosslinking in the heated mold.
Therefore, injection molding should not be defined as a process exclusively for thermoplastics. Material formulation and machine/process configuration determine whether a specific material can be injection molded.
How to Choose Between Compression, Transfer, and Injection Molding
A practical process-selection review should start with the variables that can eliminate unsuitable processes.
1. Start With the Material
Determine whether the material is:
- Thermoplastic
- Thermoset
- Elastomeric
- Composite
- A specialized medical-grade formulation
Material flow behavior, curing characteristics, thermal stability, and processing window can immediately narrow the available processes.
2. Evaluate Part Geometry
Consider:
- Overall part size
- Wall thickness
- Deep features
- Undercuts
- Inserts
- Dimensional tolerances
- Surface requirements
Complex geometries may favor processes with more controlled cavity filling, while large and comparatively straightforward parts may be suitable for compression molding.
3. Consider Production Volume
Production volume affects how much tooling complexity and automation can be economically justified.
A relatively simple mold may be appropriate when annual volume is limited. Higher volumes can justify multi-cavity tooling, automation, and shorter repeatable cycles.
4. Compare Tooling Requirements
Evaluate:
- Mold complexity
- Cavity count
- Runner and gate requirements
- Cooling or heating
- Ejection
- Slides and lifters
- Insert loading
- Maintenance requirements
The lowest initial tooling cost is not necessarily the lowest total production cost.
5. Evaluate Material Utilization
Compare:
- Charge efficiency
- Flash
- Transfer pad and runner waste
- Sprue and gate waste
- Potential hot-runner use
- Secondary trimming
This can be particularly important when processing expensive materials.
6. Check Medical Manufacturing Requirements
For medical components, the process must also support the required:
- Material documentation
- Dimensional consistency
- Clean manufacturing controls
- Traceability
- Process validation
- Sterilization compatibility
- Production scalability
When molding is part of a broader medical manufacturing program, medical device contract manufacturing may also need to be considered.
Tooling Cost and Production Economics
Tooling cost should be evaluated together with production volume rather than treated as an independent measure.
Compression molds can be relatively straightforward for suitable geometries. Transfer molds add components such as the transfer pot, plunger, runners, and gates. Injection molds can require sophisticated filling, cooling, ejection, and side-action systems depending on the part design.
A higher initial tooling investment can still be reasonable when it supports:
- Higher cavity counts
- Greater automation
- Lower labor requirements
- More consistent production
- Higher annual production volume
- More efficient cycle utilization
Conversely, simpler tooling can be more appropriate when production volume is limited or when the component does not require complex cavity filling.
The relevant comparison is therefore total production economics, not simply the initial mold price.
Material Waste and Flash
Material utilization also differs among the three processes.
Compression molding can achieve relatively efficient material utilization when the charge is accurately measured, although flash and trimming depend on the mold design and material.
Transfer molding introduces a transfer pad, sprue, runners, or other flow-system material. For thermosetting materials, this material generally cannot be remelted and returned to the process, making transfer-system waste an important consideration.
Injection molding can also generate sprue, runner, and gate waste. The amount depends on mold architecture, runner design, cavity arrangement, and whether a hot-runner system is used.
For expensive medical-grade materials, material utilization should therefore be considered alongside tooling, cycle time, labor, and production volume.
Medical Manufacturing Considerations
For medical components, molding process selection is only one part of the manufacturing decision.
Important considerations can include:
- Material and grade requirements
- Part geometry and dimensional tolerances
- Insert requirements
- Surface and cosmetic requirements
- Clean manufacturing requirements
- Production volume
- Process repeatability
- Validation requirements
- Traceability
- Sterilization compatibility
- Secondary assembly requirements
A molding process may produce a technically acceptable part but still be unsuitable for a medical production program if the material, quality controls, process validation, documentation, or production scalability do not meet the project requirements.
SeaSkyMedical can support medical manufacturing projects where injection molding and related manufacturing capabilities match the component and production requirements.
Frequently Asked Questions
What is the main difference between transfer molding and compression molding?
Compression molding places the material charge directly into the mold and uses heat and pressure to form the part. Transfer molding places the charge into a separate transfer pot and uses a plunger to force the material through runners and gates into a closed cavity.
What is the difference between transfer molding and injection molding?
Both processes use pressure-driven material flow into a closed mold, but transfer molding uses a transfer pot and plunger, while injection molding uses an injection unit to plasticize, meter, and inject the material.
Does transfer molding use runners and gates?
Yes. Transfer molds use a flow system that can include runners and gates to direct material from the transfer pot into the mold cavities. This flow system is one reason transfer molding requires more tooling components than basic compression molding.
Does transfer molding create more waste than compression molding?
It can. Transfer molding introduces a transfer pad, sprue, runners, and gates that can add material waste compared with direct compression molding. The actual difference depends on mold design, part size, charge efficiency, and material utilization.
Is transfer molding suitable for medical components?
It can be, depending on the material, part geometry, insert requirements, quality requirements, and production process. The suitability of transfer molding should be evaluated together with the medical component’s material and manufacturing requirements rather than determined by process type alone.
Can thermoset materials be injection molded?
Yes. Suitable thermoset compounds can be injection molded. The material is injected into a heated mold and then cures through a crosslinking reaction rather than simply solidifying through cooling.
Which molding process is best for high-volume production?
Injection molding is often well suited to high-volume production because it can support automated material handling, multi-cavity tooling, and repeatable cycles. However, the appropriate process still depends on material, geometry, tooling investment, and production requirements.
How does tooling cost differ among compression, transfer, and injection molding?
Compression tooling can be relatively straightforward for suitable components. Transfer tooling adds a transfer pot and material flow system, while injection molds can become highly complex when the part requires multiple cavities, slides, lifters, specialized cooling, or other advanced tooling features.
Conclusion
Transfer molding, injection molding, and compression molding each provide different combinations of material compatibility, cavity-filling behavior, tooling requirements, production efficiency, and scalability.
Compression molding can be effective for suitable thermoset, composite, and elastomer applications, particularly when relatively straightforward tooling and direct compression are appropriate.
Transfer molding introduces a transfer pot, plunger, and flow system between the molding charge and the closed cavity. This can provide greater control for inserts and more complex features while adding tooling and material-utilization considerations.
Injection molding provides a scalable production method for many thermoplastic applications and can also be used with suitable thermoset systems. Its advantages become particularly relevant when repeatability, automation, complex geometry, and production volume are important.
The most appropriate process is determined by the combination of material, geometry, tooling, production volume, cycle time, material utilization, dimensional requirements, and manufacturing controls.
For medical components, those factors should also be evaluated alongside material compatibility, cleanliness, validation, traceability, and the intended production scale. SeaSkyMedical can support medical manufacturing projects where injection molding and related capabilities match the component and production requirements.