Medical-grade low-density polyethylene (LDPE) is a flexible thermoplastic used in selected pharmaceutical packaging, medical containers, and fluid-handling applications. Its branched molecular structure contributes to its relatively low density, flexibility, and suitability for film processing and selected tubing designs.
Not every LDPE resin is suitable for medical use. Grade selection depends on the intended application, material formulation, manufacturing process, product-contact conditions, and applicable verification requirements. Packaging projects must establish barrier performance and seal integrity, while tubing projects must address dimensions, pressure performance, bending behavior, and fluid compatibility.
What Is Medical-Grade LDPE?
Low-density polyethylene is a thermoplastic polymer produced from ethylene. Compared with conventional high-density polyethylene (HDPE), LDPE generally has more branched molecular chains, which limit close molecular packing and contribute to lower density and crystallinity.
This structure helps explain LDPE’s flexibility and suitability for many films and flexible containers. However, medical grade is not a universal designation that establishes suitability for every medical application. A resin intended for pharmaceutical packaging may not be appropriate for patient-contacting tubing without further evaluation.
Key Properties of LDPE for Medical Applications
| Property | Engineering relevance | What to verify |
|---|---|---|
| Flexibility | Supports flexible films, squeeze containers, and selected tubing designs | Stiffness, deformation, recovery, and temperature-dependent performance |
| Moisture resistance | Helps limit moisture exposure in suitable packaging structures | Required moisture barrier of the complete package |
| Chemical resistance | May tolerate many aqueous solutions and selected chemicals | Chemical identity, concentration, temperature, contact duration, and applied stress |
| Heat-sealing behavior | Supports selected flexible packaging and container-closing processes | Seal strength, process window, and package integrity |
| Impact resistance | Helps some flexible products withstand handling loads | Performance under actual geometry, temperature, and loading conditions |
| Thermal behavior | Influences forming, sealing, and dimensional stability | Grade-specific processing data and finished-product performance |
These are general LDPE characteristics, not guaranteed specifications for every medical-grade resin. Application-specific performance must be established using the selected grade’s technical documentation and relevant testing.
Medical-Grade LDPE Versus General-Purpose LDPE
A medical-grade resin should be evaluated through its specific grade documentation, intended-use information, manufacturing controls, and applicable compliance declarations. The polymer name alone does not establish suitability.
For example, DOW™ LDPE 91003 HEALTH+ is a specific LDPE grade designed for blow-fill-seal processing, with listed applications including pharmaceutical packaging, vials, and ampoules. Its published data include a density of 0.927 g/cm³ and a melt index of 0.30 g/10 min under the stated test conditions.
These figures describe that particular grade, not universal LDPE specifications. When evaluating a resin, confirm its grade name, test methods, intended applications, technical data sheet, and relevant regulatory documentation.
LDPE for Medical and Pharmaceutical Packaging
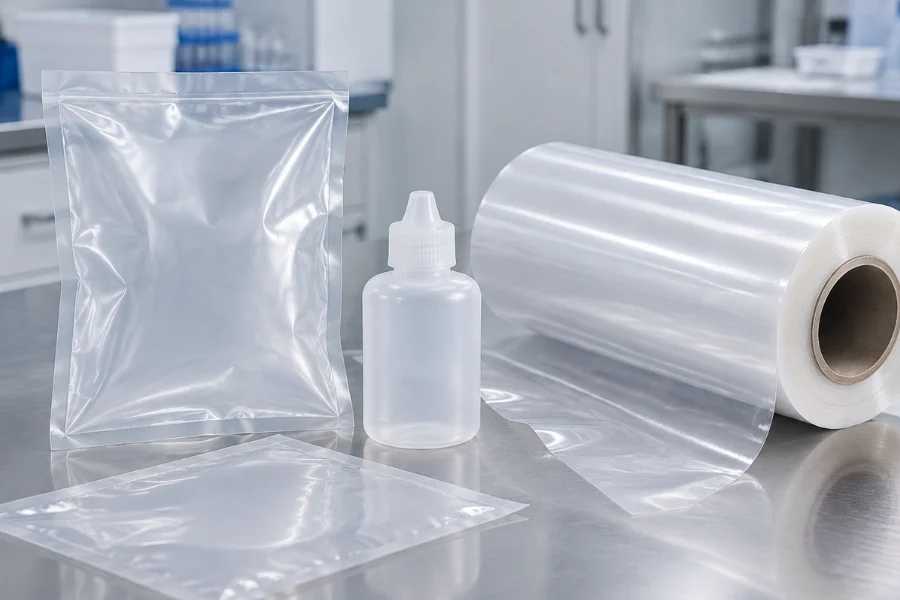
LDPE is used in selected packaging applications where flexibility, moisture resistance, and compatible processing characteristics are important. Its suitability depends on the product being protected and the performance of the complete package throughout manufacturing, storage, transport, and use.
Flexible Films, Bags, and Pouches
LDPE can serve as a film, bag or pouch material, or a layer within a multilayer packaging structure. Its heat-sealing characteristics can support package closure, but seal performance depends on the material structure and controlled processing conditions.
LDPE alone does not establish sterile-barrier performance. A package may also need to meet requirements for microbial barrier protection, mechanical integrity, and resistance to handling and distribution stresses.
For applicable terminally sterilized medical devices, ISO 11607-1 addresses materials, preformed sterile barrier systems, and packaging systems intended to maintain sterility until the point of use. It is not a universal certification of LDPE resin.
Packaging evaluation should consider the package configuration, sealing process, sterilization conditions, storage environment, and distribution requirements together.
For projects requiring packaging operations, explore SeaSkyMedical’s medical device packaging capabilities.
Pharmaceutical Bottles and Liquid Containers
Selected LDPE grades can be used in squeeze bottles, liquid containers, and other pharmaceutical packaging components. Flexibility may support dispensing, while moisture resistance can benefit certain formulations.
The key selection issue is compatibility between the formulation and the packaging material. Chemical composition and storage conditions may affect material performance or require additional compatibility studies and chemical risk assessments.
A grade used for one pharmaceutical product should not automatically be assumed suitable for another. Review the manufacturer’s application documentation, restrictions, and relevant regulatory or pharmacopoeial requirements.
Blow-Fill-Seal Packaging
Blow-fill-seal (BFS) is an integrated process in which a container is formed, filled, and sealed within a production sequence. Certain LDPE grades are designed for pharmaceutical packaging applications using BFS.
Material selection must account for melt behavior, container formation, wall-thickness distribution, sealing, product compatibility, and process consistency. Grade suitability should be confirmed under the intended manufacturing conditions rather than inferred from the polymer name alone.
Medical Packaging Evaluation Checklist
| Evaluation area | What must be established |
|---|---|
| Intended use | Whether the package is for medical supplies, a pharmaceutical product, or a sterile medical device |
| Barrier performance | Whether the complete package meets moisture, gas, light, and contamination-protection requirements |
| Product compatibility | Whether the formulation may interact with the resin, additives, or other packaging layers |
| Seal integrity | Whether the seal remains acceptable under defined processing and distribution conditions |
| Sterilization | Whether the material and package retain required performance after the intended process |
| Verification | Which tests and records are needed to support the complete packaging system |
LDPE for Medical Tubing
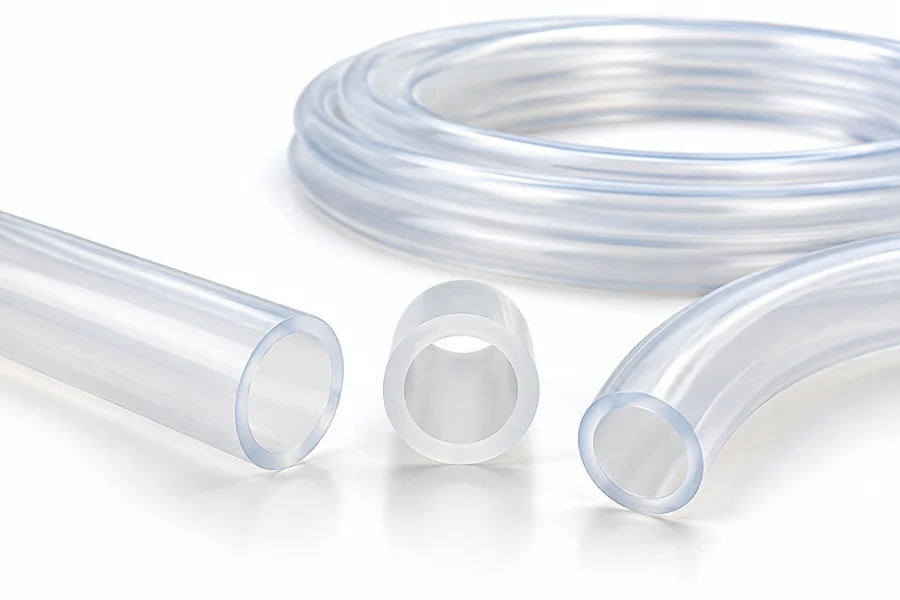
LDPE may be suitable for selected medical and laboratory tubing applications where flexibility and moisture resistance are useful. Its suitability depends on the required dimensions, mechanical performance, fluid compatibility, operating conditions, and intended use.
Tubing Dimensions and Dimensional Control
The inner diameter determines the available flow passage, while the outer diameter and wall thickness influence fit, flexibility, and mechanical performance. For a nominally circular tube:
Wall thickness = (Outer diameter − Inner diameter) / 2
Dimensional variation can affect flow, connector fit, and assembly consistency. Tubing specifications should therefore define critical dimensions and acceptable tolerances according to the component’s function.
The supplied reference book includes a general LDPE extrusion example with a nominal outer diameter of 24 mm and inner diameter of 19 mm. These are textbook process examples, not medical tubing specifications or recommended dimensions for a particular device.
Kink Resistance and Pressure Performance
Bending or compressing flexible tubing can reduce its internal flow area or interfere with fluid delivery. The extent of deformation depends on the tube geometry, material behavior, temperature, and loading conditions.
Engineering evaluation should consider:
- Minimum bend radius and expected routing
- Wall thickness and dimensional tolerances
- Operating pressure and temperature
- Material stiffness and recovery after deformation
- Connector geometry and assembly loads
- Performance after relevant chemical or environmental exposure
Pressure capability must be established for the finished tubing under defined test conditions. It cannot be inferred from resin flexibility alone. Connector fit, leakage, and pull-out resistance also depend on the mating geometry and assembly process.
Chemical Compatibility and Environmental Stress Cracking
LDPE’s general chemical resistance does not guarantee compatibility with every fluid or assembly chemical. Concentration, temperature, contact duration, mechanical stress, and exposure to cleaning agents or solvents can influence failure risk.
A 2022 study in Engineering Failure Analysis investigated environmental stress cracking in medical-grade LDPE ventilator tubing exposed to isopropanol used as an assembly aid. The researchers reproduced the failure mechanism and reported reduced failure likelihood in the investigated case when an elastomer was blended with LDPE or an alternative solvent was used.
This finding is specific to the studied material and conditions; it does not establish that isopropanol will cause every LDPE tube to fail. It demonstrates why compatibility assessments must include the manufacturing and assembly environment, not just the fluid transported during use.
For a new tubing application, evaluate relevant fluids, cleaning agents, lubricants, adhesives, and assembly aids. Where a failure could affect device function or patient safety, document the assessment and support it with appropriate testing.
Extrusion Process Considerations
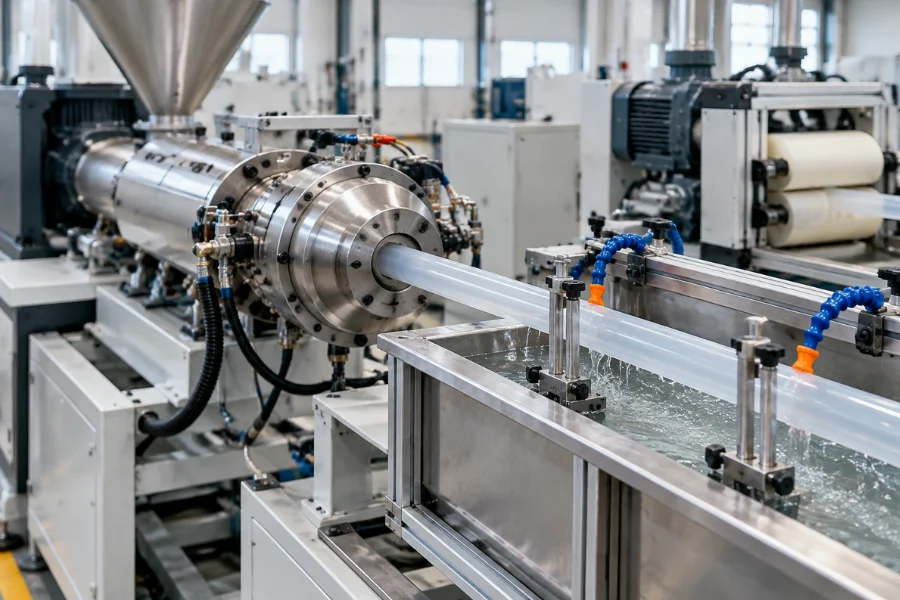
The supplied reference book identifies melt-temperature control, filtration, die geometry, sizing, cooling, and dimensional shrinkage as important factors in polyethylene tubing extrusion.
| Process variable | Potential effect on tubing | Engineering consideration |
|---|---|---|
| Melt temperature | Influences flow behavior and processing stability | Establish a suitable processing window for the selected grade and equipment |
| Die and mandrel alignment | Affects wall-thickness distribution and concentricity | Control alignment and verify dimensions around the circumference |
| Sizing and cooling | Influence shrinkage and dimensional stability | Maintain consistent cooling and measure dimensions after stabilization |
| Extrusion and take-up speeds | Affect output and final dimensions | Monitor process consistency and verify critical dimensions |
| Melt filtration | Helps control unwanted particles in the melt stream | Select filtration appropriate to the resin and process requirements |
The book’s general polyethylene extrusion temperatures and specific die setup illustrate processing principles; they are not validated medical production settings. Actual conditions must be developed for the selected resin, equipment, tubing geometry, and product requirements.
Medical manufacturing may additionally require documented controls for cleanliness, traceability, process qualification, and acceptance criteria.
Medical-Grade LDPE Compared With Other Medical Plastics
LDPE is one option within a broader range of polymers. The appropriate comparison depends on whether the application prioritizes flexibility, rigidity, heat resistance, elastic recovery, or chemical compatibility.
| Material | Potential advantages | Limitations to evaluate | When to consider it |
|---|---|---|---|
| LDPE | Flexibility, moisture resistance, heat-sealing characteristics | Lower stiffness than many rigid plastics; pressure performance depends on grade and design | Flexible packaging, selected containers, and suitable tubing |
| HDPE | Greater rigidity in many grades and good moisture resistance | Less flexible than LDPE in comparable designs | Rigid containers and components requiring stiffness |
| PP | Low density, useful chemical resistance, and good heat resistance in suitable grades | Performance depends on grade, design, temperature, and processing | Containers, closures, and selected medical components |
| EVA | Flexible formulations with tunable material properties | Performance depends on formulation, including vinyl acetate content | Selected flexible products and packaging structures |
| TPU | Elasticity, abrasion resistance, and flexible behavior across many grades | Different processing, chemical compatibility, and cost considerations | Applications requiring elastic recovery or wear resistance |
These are general engineering comparisons, not a ranking of universally suitable medical materials. Actual performance depends on the specific grade, formulation, geometry, manufacturing process, and test conditions.
When to Choose LDPE or Consider an Alternative
LDPE is worth evaluating when flexibility, moisture resistance, and film or container processing are central requirements.
A different polymer may be more appropriate when a component needs greater stiffness, higher temperature resistance, or specific elastic behavior. For example, HDPE or PP may warrant evaluation for rigid components, while TPU may be worth considering where elastic recovery or abrasion resistance is important.
SeaSkyMedical’s PP injection molding capabilities provide a relevant manufacturing reference for projects considering polypropylene components. For flexible components requiring further evaluation, see its TPU injection molding capabilities.
These service pages describe manufacturing options; they do not establish that a material is automatically suitable for a particular medical device. For broader options, review SeaSkyMedical’s medical plastic material selection resources.
Sterilization, Biocompatibility, and Material Verification
Medical-grade LDPE selection requires evidence appropriate to the intended application. A material description or supplier declaration alone does not establish the suitability of a finished medical product.
Sterilization Compatibility
Sterilization may affect a polymer’s mechanical properties, dimensions, appearance, and chemical characteristics. Changes depend on the resin grade, formulation, processing history, sterilization method, exposure conditions, and number of cycles.
Evaluate the selected grade and finished component under the intended sterilization process. Confirm that dimensions and mechanical performance remain within requirements and assess any relevant material-related risks.
Compatibility with ethylene oxide or radiation should not be generalized across all LDPE grades. Repeated sterilization should not be assumed acceptable without supporting evidence.
Biocompatibility and Patient Contact
The term medical grade does not automatically establish suitability for every type of patient contact. Biological evaluation depends on the device’s intended use, the nature and duration of contact, material composition, manufacturing processes, and condition of the finished device.
A risk-based medical device biocompatibility evaluation considers the finished device and relevant manufacturing and sterilization processes rather than relying solely on the identity of an individual polymer.
Review available biological evaluation information and determine what additional assessment is needed for the specific device. Neither a resin designation nor a generic compliance statement establishes universal FDA approval.
Extractables and Leachables
Extractables are chemical substances that can be released from a material under defined extraction conditions. Leachables are substances that migrate from a material into a product under actual or simulated conditions of use.
These issues can be important when polymers contact pharmaceutical formulations, biological products, or fluids delivered through a medical device. Assessment may need to consider formulation, additives, processing residues, contact conditions, and potential product interactions.
The appropriate analytical and toxicological evaluation depends on the application and its risk profile. Requirements should be confirmed against the applicable regulatory framework for the intended product and market.
Traceability and Change Control
Material qualification must remain linked to the approved resin and manufacturing process. Changes to the grade, formulation, supplier, processing conditions, or sterilization process may affect assumptions used during product development and verification.
OEM teams should retain relevant lot documentation, establish material and process change controls, and determine whether changes require additional testing or revalidation.
For projects requiring formal medical device verification and validation support, review SeaSkyMedical’s medical device validation and verification capabilities. The specific service scope should be confirmed for each project; this link does not imply that every LDPE grade or finished product is automatically qualified.
How to Select LDPE for a Medical Application
Use the following decision sequence to connect the intended use with the required material evidence and manufacturing controls.
| Decision stage | Key question | Evidence to review |
|---|---|---|
| Define the application | Is the material intended for packaging, a container, tubing, or a molded component? | Intended-use description, drawings, and functional requirements |
| Set performance criteria | Which dimensions, mechanical properties, barrier functions, and chemical exposures are critical? | Specifications, acceptance criteria, and test requirements |
| Verify the grade | Does the proposed resin support the intended use and manufacturing process? | Technical data sheet, applicable compliance declarations, and supplier documentation |
| Evaluate processing | Can the intended forming, sealing, assembly, and sterilization processes achieve the required performance? | Process assessment and relevant compatibility or validation results |
| Establish controls | How will material identity, lot traceability, and changes be managed? | Quality records, inspection plans, and change-control procedures |
Questions to Ask a Material Supplier
Before approving a grade, confirm:
- Which specific resin grade is proposed, and which applications does the manufacturer support?
- What technical data and applicable compliance declarations are available?
- Are there documented restrictions involving temperature, chemicals, sterilization, or product contact?
- What information is available about additives and extractables and leachables where relevant?
- What material traceability and change-notification controls are available?
- What additional testing is needed to qualify the finished component or packaging system?
Frequently Asked Questions About Medical-Grade LDPE
Is LDPE safe for medical use?
LDPE can be suitable for selected medical and pharmaceutical applications when the specific grade and finished product meet applicable requirements. Suitability depends on intended use, material formulation, contact conditions, manufacturing processes, and relevant biological or chemical evaluations.
Is medical-grade LDPE different from standard LDPE?
Medical-grade LDPE is intended for defined healthcare or pharmaceutical applications and should be supported by documentation appropriate to that use. Formulation controls, manufacturing controls, and compliance information vary by supplier and grade. Industrial LDPE should not be assumed suitable for medical use without further evaluation.
Can LDPE be used for medical tubing?
Selected LDPE grades may be suitable when dimensions, pressure performance, bending behavior, and chemical compatibility meet the design requirements. Patient-contacting or fluid-delivery applications may require additional evaluation based on the device’s intended use and risk profile.
Can LDPE withstand sterilization?
Compatibility depends on the specific resin grade, sterilization method, exposure conditions, and finished product. Evaluate the selected material and component under the intended process rather than assuming that all LDPE grades behave alike.
Is LDPE suitable for sterile medical packaging?
LDPE may be used in selected packaging structures, but suitability depends on the complete package design, sealing process, sterilization method, and intended use. For applicable terminally sterilized medical devices, the packaging system must meet the relevant requirements for maintaining sterility until use.
How should a medical-grade LDPE resin be verified?
Review the resin manufacturer’s technical data sheet, intended-use documentation, applicable compliance declarations, and material traceability information. Determine what additional testing is needed for the finished component or packaging system, including chemical compatibility, biological evaluation, or sterilization-related verification where applicable.
Medical Manufacturing Support for OEM Projects
For OEM projects, material selection should be coordinated with component design, manufacturing, assembly, and verification requirements. Early design-for-manufacturability reviews can identify dimensional constraints, material compatibility concerns, and process risks before tooling and production commitments are made.
SeaSkyMedical provides medical manufacturing support, including injection molding and medical device packaging. Depending on the project scope, these capabilities may be relevant when an OEM requires support with component manufacturability or packaging operations.
Explore SeaSkyMedical’s medical device contract manufacturing capabilities for manufacturing support options. For packaging-related requirements, see its medical device packaging service page.
The starting point for a new project is a defined application, documented performance requirements, and evidence supporting the proposed material grade. These inputs help determine whether LDPE is appropriate or whether another polymer should be evaluated.