Building a clean room requires a controlled enclosure, properly designed air filtration and airflow systems, and procedures that limit contamination during operation. Installing HEPA filters alone does not make a room compliant with a specified cleanliness classification.
To make a clean room, define the process requirements, select the required cleanliness level, design the layout and HVAC system, construct the enclosure, and test the completed facility before production begins.
This guide focuses on industrial cleanroom construction and setup, particularly for medical device manufacturing and assembly. It does not cover residential clean-air rooms for wildfire smoke protection or replace project-specific engineering design.
What Is a Clean Room?
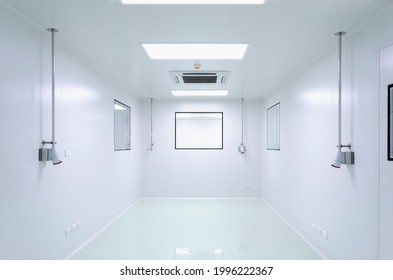
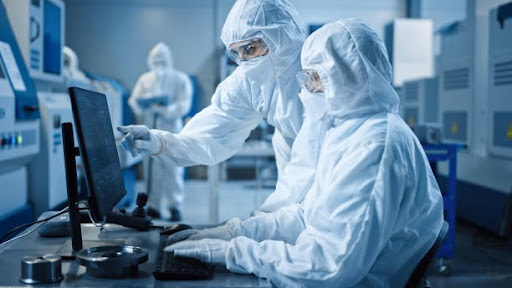
A clean room, also called a cleanroom, is a controlled environment designed to maintain specified concentrations of airborne particles. Depending on the process, it may also control temperature, humidity, pressure differences and other environmental conditions.
Clean rooms are used in medical device manufacturing, pharmaceutical production, electronics, biotechnology and other operations where airborne contamination can affect product quality.
ISO 14644-1 classifies cleanrooms according to airborne particle concentrations at specified particle sizes. Meeting an ISO cleanliness classification does not automatically mean the room is sterile or that products manufactured inside it are free from contamination.
Positive-Pressure vs. Negative-Pressure Cleanrooms
Positive-pressure cleanrooms maintain higher pressure than adjacent areas, encouraging air to move outward through leakage paths. This helps limit the entry of less-clean air and is commonly used when product protection is the primary objective.
Negative-pressure rooms maintain lower pressure than surrounding spaces, encouraging air to move inward. They may be used where containment of airborne hazards is necessary.
Pressure direction is a design decision, not a cleanliness classification. Some facilities require different pressure relationships across multiple rooms to protect products, personnel and surrounding areas.
How to Build a Clean Room Step by Step
A cleanroom project typically progresses from defining requirements to engineering design, construction, system commissioning and performance verification.
The following six steps provide a practical sequence for industrial cleanroom construction. Each stage should produce documented information that can be reviewed before the project advances.
Step 1. Define the Cleanroom Requirements
Identify the manufacturing activities, products and contamination risks that justify the controlled environment.
Establish the required airborne particle classification, operating conditions, personnel occupancy, material flow and any additional environmental controls.
Document these requirements in a user requirement specification (URS) or equivalent project specification.
Key deliverable: An approved specification describing what the cleanroom must achieve and under which operating conditions.
Step 2. Design the Layout and HVAC System
Develop a layout showing equipment locations, personnel access, material transfer routes, controlled zones and maintenance access.
Select the filtration strategy, airflow arrangement, room pressure relationships, heating and cooling capacity, and any required process exhaust.
Equipment heat loads, particle generation and available building utilities should be evaluated before finalizing the mechanical design.
Key deliverable: Coordinated room layouts, airflow design criteria, equipment requirements and utility specifications.
Step 3. Construct the Cleanroom Enclosure
Install the walls, ceilings, floors, doors and necessary utility connections according to the approved design.
Construction activities should minimize dust accumulation and protect components intended for the controlled environment.
Inspect panel joints, doors and service penetrations for sealing defects before the final cleaning and system startup.
Key deliverable: A completed, cleanable enclosure with inspected construction details and installed utilities.
Step 4. Install and Commission the Air Systems
Install the specified filters, fans, ductwork, controls and monitoring instruments.
Adjust supply, return and exhaust airflow to establish the required pressure relationships and environmental conditions.
Verify the operation of the control system and perform the applicable filter integrity and airflow tests.
Key deliverable: Commissioned mechanical systems with recorded operating conditions and initial test results.
Step 5. Test and Qualify the Cleanroom
Verify that the completed facility meets its specified performance requirements.
Testing may include airborne particle classification, airflow measurements, pressure differential verification, filter integrity testing and temperature or humidity checks.
ISO 14644-3 provides methods for relevant cleanroom tests. Additional qualification activities may be necessary for regulated manufacturing processes.
Key deliverable: Documented test results, identified deviations and evidence that the facility meets its approved acceptance criteria.
Step 6. Establish Operating and Maintenance Procedures
Develop procedures for personnel entry, gowning, material transfer, cleaning, environmental monitoring and equipment maintenance.
Define how monitoring results will be reviewed and how deviations will be investigated.
Establish change-control and requalification criteria for modifications that may affect cleanroom performance.
Key deliverable: Approved operating procedures, a monitoring plan and a preventive maintenance program.
Why Do You Need a Clean Room?
Cleanroom manufacturing helps control airborne contamination that could affect exposed products, sensitive assemblies or critical production processes.
For medical device manufacturing, potential contamination sources include personnel, equipment movement, material handling, maintenance activities and the surrounding production environment.
A controlled manufacturing area can reduce exposure to these sources when its environmental systems are supported by suitable operating procedures.
However, cleanroom classification does not replace other manufacturing controls.
For example, contaminated resin can introduce foreign material into molded components, while insufficient drying of moisture-sensitive polymers can cause molding defects. Neither problem is necessarily prevented by HEPA filtration.
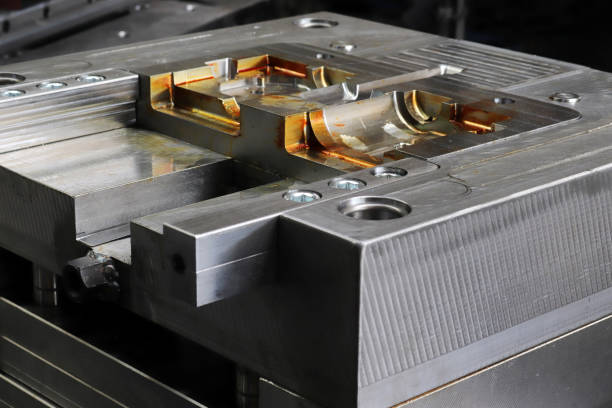
Likewise, debris remaining in a mold cavity can become embedded in subsequent molded parts.
The need for cleanroom manufacturing therefore depends on product requirements, process exposure, contamination risks and applicable quality or regulatory obligations.
Not every medical device component requires the same cleanroom classification, and some manufacturing operations may not require a classified cleanroom.
Things to Consider When Building a Clean Room
The construction sequence establishes how a cleanroom project progresses. The following engineering considerations determine whether the resulting facility can meet its intended performance requirements.
Application and Cleanroom Requirements
The manufacturing application should determine the required environmental controls.
A cleanroom used for medical device assembly may have different requirements from one used for injection molding, pharmaceutical processing or electronics production.
The selection process should begin by identifying where the product is exposed and what types of contamination could affect its quality.
For example, a molded component that remains protected throughout production may have different environmental needs from a component exposed during assembly or packaging.
This assessment should consider the product’s intended use, cleanliness specifications, subsequent processing and contamination-control measures already present in the manufacturing process.
A more stringent cleanliness classification should not be selected solely because it appears to offer greater protection. Higher classifications can increase filtration, airflow, energy and maintenance requirements without necessarily addressing the actual contamination risk.
Cleanroom Construction Types
Cleanrooms can be constructed as permanent facilities, modular enclosures or localized clean-air installations.
| Construction Type | Main Characteristics | Suitable Applications |
|---|---|---|
| Permanent cleanroom | Integrated with the building structure and mechanical services | Facilities with established layouts and long-term production requirements |
| Modular cleanroom | Uses prefabricated wall and ceiling systems | Projects requiring relatively flexible installation or future layout changes |
| Localized clean-air installation | Provides controlled airflow around a defined operation | Processes where only a limited critical area requires enhanced airborne particle control |
The choice depends on equipment dimensions, building constraints, process requirements, service access and future production changes.
A localized clean-air installation should not be assumed to provide the same protection as a fully classified room. Its performance must be evaluated for the intended operation.
Clean Room Classification
ISO 14644-1 defines airborne particle cleanliness classes based on maximum permitted particle concentrations at specified particle sizes.
Lower ISO class numbers represent more stringent airborne particle cleanliness requirements.
The required classification should be determined from the manufacturing process rather than from the industry name alone.
For example, ISO Class 7 and ISO Class 8 may be specified for certain controlled manufacturing activities, but neither is a universal requirement for medical injection molding.
When selecting a classification, consider:
- Whether the product is exposed to the surrounding air.
- The contamination sensitivity of exposed surfaces or assemblies.
- The number and activity level of personnel.
- Particle generation from equipment and materials.
- Additional cleaning, packaging or contamination-control processes.
The required occupancy state must also be defined.
A cleanroom may be classified under as-built, at-rest or operational conditions. These states describe different levels of equipment and personnel activity.
A room that meets its specified classification while empty may not maintain the same particle concentration during full production.
The design must therefore account for the conditions under which cleanliness is required.
High-Efficiency Particulate Air (HEPA) Filters
HEPA filters remove airborne particles from the air passing through the filter media and are widely used in cleanroom ventilation systems.
A commonly cited HEPA performance specification is 99.97% efficiency for 0.3-micrometer particles. Other filter standards and classifications use different test methods and performance criteria, so filter selection must follow the applicable specification.
Filter efficiency is only one part of cleanroom performance.
Air can bypass a filter through damaged media, poorly sealed frames or defective housings. Installed filter integrity testing helps identify these problems.
The filtration system should also provide sufficient airflow to the required areas.
A high-efficiency filter cannot compensate for poorly distributed air, excessive particle generation or contamination introduced directly into a critical process.
Filter access and replacement requirements should be considered during the design stage.
Recirculation Air System and Air Balance
The cleanroom ventilation system must supply sufficient filtered air to control particle concentrations and maintain the required environmental conditions.
The appropriate airflow strategy depends on room geometry, equipment layout, contamination sources and the required cleanliness level.
Nonunidirectional airflow systems use filtered air to dilute and remove airborne particles through a combination of supply and return airflow.
Unidirectional airflow systems direct clean air across a controlled area and may be used where more stringent local particle control is required.
Air changes per hour (ACH) can support preliminary sizing of some nonunidirectional airflow systems, but an ACH value alone does not establish compliance with an ISO cleanliness classification.
Equipment placement can obstruct airflow and create areas where particles are not effectively removed.
Supply and return locations should therefore be evaluated in relation to actual production equipment and personnel movement.
The system must also balance supply, return, exhaust and makeup airflow.
If process exhaust increases without an appropriate supply or makeup-air response, room pressure may fall below its intended level even though the supply filters remain functional.
Clean Room Pressurization
Pressure differences help control the direction of airflow between adjacent spaces.
Positive pressure is commonly used when the objective is to protect products from contamination entering from surrounding areas.
Negative pressure may be required when the priority is containing airborne hazards.
The appropriate pressure difference depends on room leakage, door operation, airflow stability and the requirements of the process.
A larger pressure difference is not automatically better.
Excessive pressure can make doors difficult to operate or create unnecessary demands on the ventilation system.
Pressure relationships should remain stable during normal operating conditions, including expected door movements and equipment exhaust changes.
Airlocks or controlled transition spaces may be appropriate where personnel and materials move between areas with different environmental requirements.
Structure, Room Space and Equipment Layout
The cleanroom layout should support manufacturing operations while minimizing unnecessary contamination pathways.
Personnel, incoming materials, production equipment and finished products should be arranged to reduce avoidable crossings and handling.
For medical injection molding, the layout may need to accommodate resin feeding, mold changes, automated part removal, inspection and packaging.
Equipment dimensions alone are insufficient for space planning.
Injection molding machines require clearance for mold opening, tooling replacement, maintenance and material handling. Automated systems may also need additional operating and service space.
Critical operations should be protected from unnecessary traffic and frequent door opening.
The layout should also allow maintenance personnel to access equipment without repeatedly disturbing areas where exposed products are handled.
Cleanroom Construction Materials
Cleanroom construction materials should provide durable, cleanable surfaces that minimize particle shedding.
The selection should account for cleaning chemicals, equipment loads, mechanical damage and maintenance requirements.
| Component | Main Design Considerations |
|---|---|
| Walls | Smooth surfaces, sealed joints, cleaning compatibility and impact resistance |
| Ceilings | Secure panels, sealed penetrations and access to filtration or services |
| Floors | Wear resistance, cleaning compatibility, equipment loads and suitable transitions |
| Doors | Appropriate seals, cleanable surfaces and reliable operation |
| Utility penetrations | Sealing, accessibility and control of unintended leakage paths |
Coated metal panels, modular wall systems and resin-based flooring may be appropriate depending on the project.
However, material performance depends on installation details as well as product selection.
Unsealed penetrations, damaged joints and difficult-to-clean corners can create contamination-control problems even when the main surfaces are suitable.
Where frequent cleaning is required, details such as coved floor transitions and sealed service openings may improve cleanability.
Temperature and Humidity Control
Temperature and humidity should be controlled according to manufacturing requirements, equipment needs and personnel conditions.
Temperature variation can affect dimensional measurement, equipment operation and some manufacturing processes.
Humidity can influence static charge accumulation, condensation and moisture-sensitive materials.
In medical injection molding, some polymers require drying before processing.
Polycarbonate, polyamides and other moisture-sensitive materials can develop processing defects or experience degradation when their moisture content exceeds the applicable material requirements.
However, cleanroom humidity control does not replace resin drying.
A material dryer controls resin moisture before molding, while the cleanroom HVAC system controls the surrounding environment.
These systems should be specified independently and coordinated where necessary.
Personnel Access and Product Storage
Personnel and material movement should be controlled to reduce contamination entering critical production areas.
Depending on the cleanliness requirements, a facility may use gowning rooms, airlocks, designated storage areas and controlled material transfer procedures.
Cleanroom garments should be selected according to the contamination risks and operating conditions.
Materials entering the cleanroom may require removal of external packaging, cleaning or transfer through designated access points.
Finished products should be handled and stored according to their exposure sensitivity.
The objective is to maintain an appropriate separation between uncontrolled handling activities and critical manufacturing operations.
Electrostatic Discharge (ESD)
Electrostatic discharge control may be necessary for sensitive electronics or processes affected by static electricity.
Static charge can also attract particles to surfaces, making electrostatic behavior relevant to some cleanroom applications.
Grounding, suitable materials and ionization systems may be used where justified by the process.
However, ESD controls should be selected according to actual product and equipment requirements rather than treated as mandatory for every cleanroom.
Measurement and Instrumentation
Cleanroom performance must be measured under defined conditions.
The required instruments depend on the classification, environmental specifications and monitoring plan.
| Measurement | Purpose |
|---|---|
| Airborne particle counting | Verify particle concentrations against the specified classification |
| Airflow volume or velocity | Confirm ventilation and air distribution performance |
| Differential pressure | Monitor airflow relationships between controlled spaces |
| Temperature and humidity | Verify environmental operating conditions |
| Installed filter integrity | Detect leakage through or around installed filters |
Initial classification testing and routine monitoring serve different purposes.
Classification testing establishes whether the cleanroom meets its specified airborne particle limits under defined conditions.
Routine monitoring helps identify changes during continued operation.
A monitoring plan should specify locations, measurement frequency, alert or action limits where appropriate, and procedures for investigating deviations.
Operations, Maintenance and Cleaning Compatibility
Cleanroom equipment and building systems must remain accessible for maintenance.
Filters, fans, sensors, dampers and production equipment may require periodic inspection, repair or replacement.
Where practical, maintenance-intensive components should be accessible without unnecessarily disturbing critical clean areas.
Cleaning procedures should also be compatible with the room’s construction materials and equipment.
A chemical that is suitable for one surface may damage another through corrosion, coating deterioration or seal degradation.
The cleaning program should define approved agents, methods, equipment and responsibilities.
Maintenance or cleaning activities that could affect environmental performance may require additional inspection or testing before normal production resumes.
Cleanroom Standards and Testing Requirements
Several standards address different aspects of cleanroom design, classification, testing and monitoring.
They should not be treated as interchangeable.
| Standard | Main Scope | Relevance to Cleanroom Projects |
|---|---|---|
| ISO 14644-1 | Classification of air cleanliness by particle concentration | Defines airborne particle cleanliness classes |
| ISO 14644-2 | Monitoring to provide evidence of cleanroom performance | Supports ongoing environmental monitoring |
| ISO 14644-3 | Cleanroom test methods | Provides methods for relevant performance tests |
| ISO 14644-4 | Design, construction and startup | Supports the cleanroom project lifecycle |
| ISO 13485 | Medical device quality management systems | Provides quality management context for applicable medical device manufacturing |
The ISO 14644 series addresses cleanroom-related environmental performance, while ISO 13485 addresses medical device quality management systems.
Neither should be interpreted as requiring every medical device manufacturing operation to use the same ISO cleanroom classification.
Cleanroom Classification vs. Facility Qualification
Airborne particle classification verifies whether particle concentrations meet the specified ISO class under defined conditions.
Installed filter integrity testing checks for leakage through the installed filtration system.
Facility qualification evaluates whether the completed facility meets its documented design and performance requirements.
Manufacturing process validation is a separate activity that may be required to demonstrate that a process can consistently produce acceptable results.
These activities can support one another, but passing a cleanroom particle classification test does not automatically validate the manufacturing process.
If a cleanroom fails an acceptance test, the investigation should address the specific failure.
For example, an unexpected particle count may require checking particle sources, airflow distribution, cleaning conditions or filtration performance.
A pressure differential failure may instead indicate problems with air balance, leakage or control settings.
Corrective actions should be verified through appropriate retesting.
Cleanroom Considerations for Medical Injection Molding
Medical injection molding introduces process-specific contamination risks that should be addressed during cleanroom design and operation.
The required controls depend on the component, its intended use and the manufacturing steps performed within the controlled area.
Mold Cleaning and Particle Control
Molded components may be exposed to particles generated by mold wear, trimming, tooling maintenance and equipment movement.
Debris remaining in a mold cavity can also become embedded in subsequent molded parts.
Mold cleaning procedures should therefore be selected according to tooling requirements and cleanroom contamination-control practices.
Unrestricted compressed-air blowing can disperse particles and should not automatically be used as a cleanroom cleaning method.
Where compressed air is required, its quality and application should be controlled according to the process requirements.
Material Preparation and Handling
Resin storage, drying, conveying and feeding can introduce contamination if materials and handling systems are not adequately controlled.
Material preparation equipment may be located outside the most critical clean area where the process layout permits controlled transfer into molding equipment.
This can reduce unnecessary equipment and personnel activity near exposed molded components.
Resin inspection and drying remain necessary process controls regardless of the room’s ISO classification.
Part Removal, Inspection and Packaging
Molded parts may become exposed to airborne contamination during ejection, transfer, inspection and packaging.
Automated handling can reduce direct operator contact, but conveyors, robots and associated equipment must also be evaluated as potential contamination sources.
The cleanroom layout should minimize unnecessary transfers between controlled and uncontrolled areas.
For components with defined cleanliness requirements, packaging and downstream handling should preserve the cleanliness achieved during manufacturing.
Process Exhaust and Equipment Maintenance
Injection molding equipment may generate heat, vapors or other process emissions depending on the polymer and operating conditions.
These emissions should be assessed separately from the airborne particle contamination controlled by the cleanroom filtration system.
Where necessary, dedicated process exhaust should be coordinated with the room’s HVAC and pressure-control systems.
Mold changes and equipment maintenance can also introduce particles and disturb normal production conditions.
The facility should establish procedures for protecting exposed products and restoring the required environmental conditions after such activities.
Conclusion
Making a clean room requires defined cleanliness requirements, coordinated layout and HVAC design, suitable construction materials, documented testing and ongoing contamination control.
For medical injection molding, the cleanroom must also account for material handling, tooling maintenance, part exposure and packaging. The appropriate design is the one that meets the documented process requirements under actual operating conditions, rather than simply selecting the most stringent available cleanliness classification.