Injection molding, also spelled injection moulding in British English, is a manufacturing process used to produce repeatable parts by injecting molten material into a shaped mold cavity. It is most commonly associated with thermoplastics, although specialized processes can also mold thermosets, elastomers, silicone and other materials.
The process is well suited to complex geometries and production where dimensional consistency and repeatability are important. Once the mold and process are established, the molding cycle can be repeated efficiently across large production volumes.
This guide explains how injection molding works, its main methods, materials, process parameters, tooling, design considerations, common defects, applications and production costs.
What Is Injection Molding?
Injection molding is a manufacturing method in which material is heated or otherwise prepared to reach a flowable state, injected under pressure into a closed mold cavity, allowed to solidify and then ejected as a finished or near-finished part.
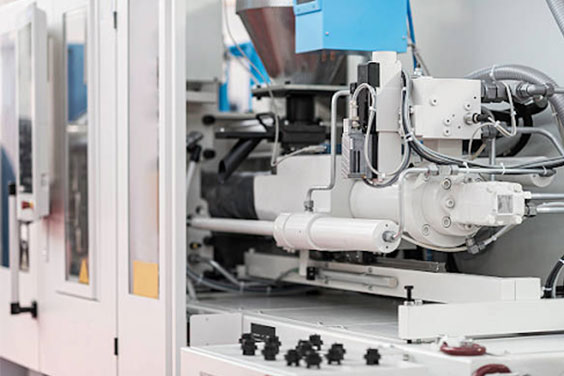
In conventional plastic injection molding, polymer pellets are plasticized inside a heated barrel by a rotating screw. The screw then moves forward to inject the melt into the mold, where pressure is maintained during the early stages of cooling before the solidified part is ejected.
This repeatable cycle makes injection molding particularly useful when many parts with the same geometry must be manufactured consistently.
Thermoplastics are the most commonly injection-molded materials. The differences between thermoplastics and thermosets affect how they respond to heat and how they must be processed.
How Does the Injection Molding Process Work?
The injection molding process includes material preparation, plasticization, mold filling, packing, cooling and ejection. Each stage influences the consistency and quality of the molded part.
1. Material Preparation and Plasticization
Before molding, the selected resin is prepared according to its processing requirements. Moisture-sensitive polymers may require drying because excess moisture can contribute to surface defects, bubbles, degradation or changes in material properties.
Plastic pellets enter the barrel through the hopper. As the screw rotates, barrel heating and shear convert the solid material into a sufficiently uniform melt and prepare the required shot volume.
2. Mold Clamping and Injection
The mold closes and the clamping system holds its two halves together. The screw then moves forward, forcing molten polymer through the nozzle, runner and gate into the cavity.
The melt must fill the geometry before cooling restricts further flow, making part geometry, material flow behavior and mold design important to successful filling.
3. Packing and Holding
After the cavity fills, the polymer begins to contract as it cools. Packing and holding pressure continue feeding material into the cavity while the gate remains open enough to transmit pressure.
Appropriate packing helps compensate for volumetric shrinkage and supports dimensional consistency. Insufficient packing can contribute to sink marks, voids and excessive shrinkage.
4. Gate Freeze and Cooling
Cooling begins as soon as the polymer contacts the mold surfaces. Once the gate freezes, additional holding pressure can no longer feed material effectively into the cavity.
Cooling continues until the component becomes rigid enough to be removed without unacceptable deformation. Part thickness, polymer properties, mold temperature and cooling-system design all influence the required cooling time.
5. Mold Opening and Part Ejection
After sufficient cooling, the mold opens and ejector pins, plates or other mechanisms remove the component.
Depending on the product, molded parts may then undergo trimming, machining, printing, assembly, cleaning or packaging. Medical components may require additional controlled handling or manufacturing steps according to product requirements.
Main Types of Injection Molding
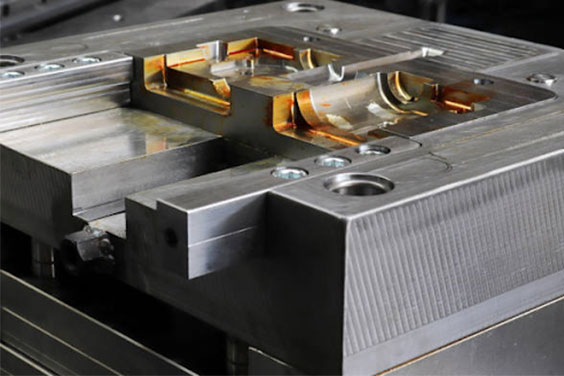
The term injection molding methods covers processes developed for different materials, geometries, part sizes and multi-material requirements.
Conventional Plastic Injection Molding
Conventional thermoplastic injection molding provides the baseline process for many molded plastic components. Its main advantage is the ability to repeatedly reproduce complex geometry using a wide range of thermoplastic resins.
Materials such as PP, PE, ABS, PC, POM and polyamides can be processed this way, although each requires an appropriate processing window and mold design.
Micro Injection Molding
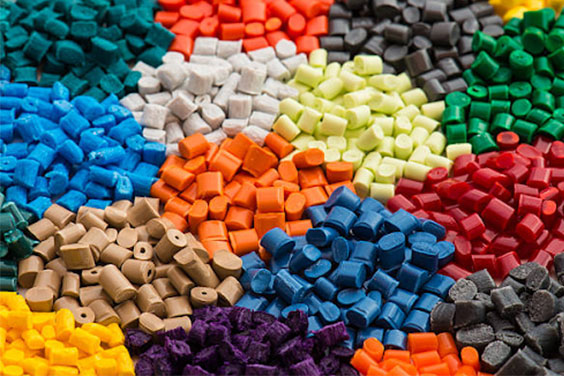
Micro injection molding is used for very small components or parts containing micro-scale features.
Small cavities, thin features and low shot weights increase the importance of tooling accuracy, filling behavior, material preparation and dimensional control. The process is used for selected medical, diagnostic and electronic components.
Overmolding
Overmolding molds one material over a previously formed substrate. It can combine different functional properties, such as a rigid structure with a softer elastomeric surface.
Material compatibility, adhesion, substrate geometry and processing conditions must be considered during development.
Insert Molding
Insert molding places a premanufactured component into the mold before polymer is injected around it.
Metal pins, threaded inserts and other functional components can therefore be integrated into a molded part, potentially reducing subsequent fastening or assembly operations.
Liquid Silicone Rubber Injection Molding
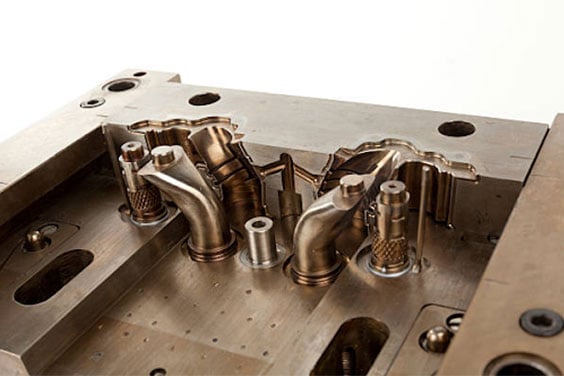
Liquid silicone rubber injection molding uses metered liquid silicone components that are mixed and injected into a heated mold, where the material cures.
Unlike conventional thermoplastics, LSR solidifies through curing rather than simply cooling from a molten state.
Gas-Assisted Injection Molding
Gas-assisted injection molding introduces pressurized gas during molding to form hollow sections or assist the molding of suitable thick geometries. It can reduce material use and help manage sink or warpage when the part geometry and gas path are designed appropriately.
Thin-Wall Injection Molding
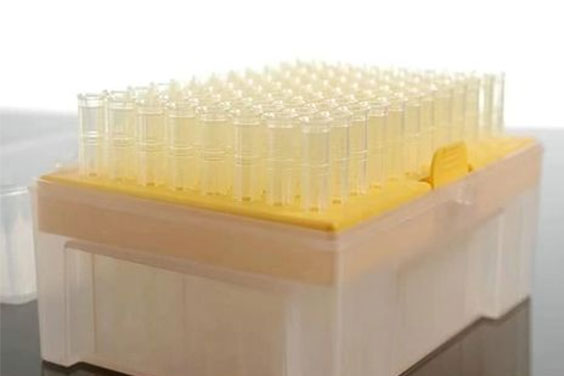
Thin-wall injection molding is used for parts with thin sections and demanding flow-length-to-thickness relationships. Because these sections cool quickly, material flow, gate design, filling speed and mold conditions require careful control.
Multi-Shot and Multi-Material Molding
Multi-shot molding combines two or more materials or colors through coordinated molding cycles. It can integrate different surface, structural or functional characteristics while reducing some downstream assembly operations.
Key Injection Molding Process Parameters
Injection molding quality depends on interactions among temperature, pressure, speed and time. Appropriate settings depend on the polymer, geometry, mold and equipment rather than on universal values.
Melt and Mold Temperature
Barrel temperature and screw shear help melt and plasticize the resin. Insufficient temperature can restrict flow, while excessive temperature or residence time can degrade heat-sensitive materials.
Mold temperature affects both cavity filling and cooling. For semicrystalline polymers, it can also influence crystallization and resulting part properties.
Injection Pressure and Speed
Injection pressure provides the force required to move the melt through the nozzle, feed system and cavity. Required pressure varies with material viscosity, wall thickness, flow length, gate geometry and temperature.
Injection speed controls how quickly the cavity fills. Thin sections often require faster filling because the melt has less time before cooling restricts flow.
Packing Pressure and Holding Time
Packing pressure compensates for material shrinkage while the gate can still transmit pressure into the cavity. Once the gate freezes, extending holding time generally provides little additional packing benefit.
Cooling Time
Cooling must continue until the component is sufficiently rigid for ejection. Material thermal behavior, part thickness, mold temperature and cooling-channel design all influence this stage and the overall cycle time.
Back Pressure
Back pressure acts against the screw during material recovery. It can improve melt mixing and temperature uniformity, but excessive back pressure may increase shear heating, residence time and cycle time.
Common Injection Molding Materials
Material selection must consider both final part requirements and molding behavior. Strength, stiffness, chemical resistance, temperature performance, moisture behavior and shrinkage can all influence the decision.
| Material | Typical Characteristics | Processing Considerations |
|---|---|---|
| Polyethylene (PE) | Chemical resistance, flexibility, relatively low cost | Grade and density affect stiffness, shrinkage and processing |
| Polypropylene (PP) | Chemical resistance, low density, fatigue resistance | Crystallization and shrinkage require dimensional consideration |
| ABS | Toughness, surface quality, dimensional performance | Moisture and temperature control affect molding quality |
| Polycarbonate (PC) | Impact resistance, transparency in suitable grades, dimensional stability | Requires appropriate drying and temperature control |
| Polyoxymethylene (POM) | Stiffness, low friction, wear resistance | Processing temperature and residence time require control |
| Polyamide (PA/Nylon) | Strength, wear resistance, temperature performance | Moisture absorption makes material conditioning important |
| PMMA | Optical clarity, surface appearance, weatherability | Surface defects and flow behavior require appropriate processing |
| PEEK | High-temperature and chemical resistance, high mechanical performance | Requires substantially higher processing temperatures than commodity polymers |
For medical components, resin selection may also depend on biocompatibility requirements, sterilization method, chemical exposure, traceability and the availability of an appropriate medical-grade formulation. These requirements should be evaluated for the specific device and intended use rather than assumed from the polymer family alone.
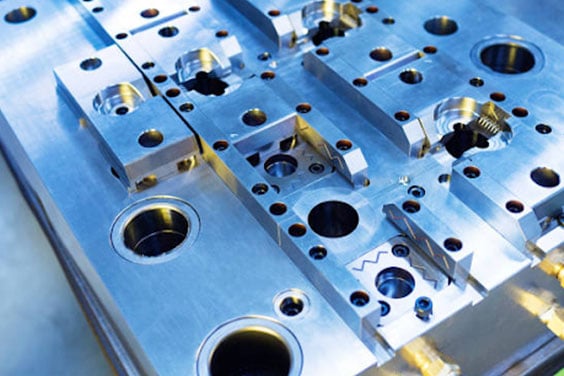
Injection Mold and Machine Components
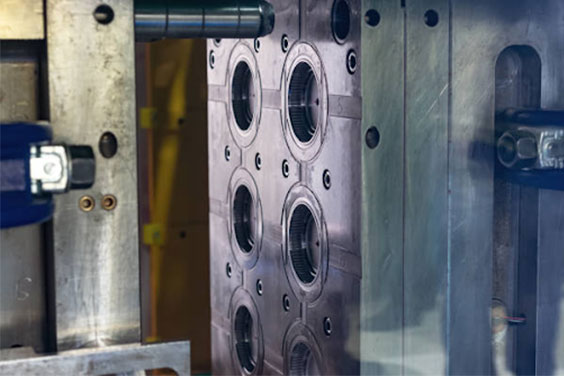
The injection molding machine and mold operate as one manufacturing system. The machine generally contains an injection unit, which plasticizes and delivers the material, and a clamping unit, which closes the mold and resists injection forces.
The mold contains several functional systems:
- Core and cavity: Form the geometry of the molded component.
- Sprue, runner and gate: Direct molten polymer into the cavity.
- Cooling system: Removes heat and helps control the cooling cycle.
- Ejection system: Removes the cooled component after the mold opens.
- Venting: Allows displaced air and gases to escape during filling.
- Mold base and guiding components: Support and align the mold assemblies.
Tool material also depends on the application. Aluminum tooling can suit some prototype or lower-volume programs, while tool steels are generally better suited to demanding production volumes, abrasive materials and longer tool-life requirements.
Design Considerations for Injection-Molded Parts
A part that can be modeled in CAD is not automatically suitable for reliable injection molding. Geometry affects filling, cooling, shrinkage, ejection, tooling complexity and cycle time.
| Design Factor | Why It Matters |
|---|---|
| Wall thickness | Large thickness changes can cause uneven cooling, sink marks, voids and warpage |
| Draft | Helps the molded part release from the tooling without excessive ejection force |
| Ribs and bosses | Add stiffness or assembly features without unnecessarily thickening the main wall |
| Undercuts | May require slides, lifters or other tooling mechanisms |
| Gate location | Influences flow length, weld lines, air trapping, packing and gate vestige |
| Tolerances | Tight tolerances may require greater control of material shrinkage, tooling dimensions and process variation |
Where geometry permits, relatively uniform wall thickness helps create more predictable filling and cooling. Draft should be established according to factors such as material, texture and feature depth rather than treated as one fixed value.
Critical dimensions should also be identified early. Material shrinkage, cavity position, geometry and processing variation all influence dimensional capability, so not every feature should automatically receive the tightest possible tolerance. These considerations are also important when managing injection molding shrinkage.
Common Injection Molding Defects
Molding defects usually result from interactions among material behavior, part geometry, mold design and process conditions. Diagnosis should therefore focus on the underlying mechanism rather than changing one machine setting in isolation.
| Defect | Common Contributing Factors |
|---|---|
| Sink marks | Thick sections, inadequate packing, localized material mass |
| Warpage | Uneven cooling, differential shrinkage, material orientation |
| Short shots | Restricted flow, insufficient pressure or speed, premature freezing |
| Flash | Excessive cavity pressure, mold parting-line or shutoff issues |
| Weld lines | Separate flow fronts meeting around holes or other geometry |
| Voids | Thick sections, shrinkage and insufficient packing |
| Burn marks | Trapped gas, inadequate venting or excessive local heating |
A tooling change may be appropriate in one case, while material preparation, gate design or process adjustment may solve another.
Advantages and Limitations of Injection Molding
Injection molding becomes particularly valuable when the part design and production requirements justify dedicated tooling.
Advantages
- High repeatability: Established tooling and process conditions support consistent production across large quantities.
- Complex geometry: Ribs, bosses, molded-in details and other features can often be produced in one cycle.
- Production efficiency: Automated cycles support efficient repeated manufacturing.
- Material flexibility: Numerous thermoplastics and specialized molding processes are available for different performance requirements.
- Economies of scale: Tooling investment can be distributed across more parts as production volume increases.
Limitations
- Upfront tooling investment: Mold design, machining, testing and qualification require initial cost and lead time.
- Design constraints: Wall thickness, draft, undercuts, gate location and ejection must be considered during development.
- Costly late design changes: Significant geometry changes after tooling may require mold modification or replacement.
- Low-volume economics: CNC machining, additive manufacturing or other methods may be more economical for prototypes and some small production quantities.
Injection molding and CNC plastic machining therefore serve different manufacturing requirements rather than one process being universally better.
Applications of Injection Molding
Injection molding is used across industries because it combines repeatable production, complex geometry and broad material availability.
Medical Devices and Pharmaceuticals
Injection molding is used for medical and diagnostic products such as housings, connectors, fluid-management components, laboratory consumables and selected surgical-device components.
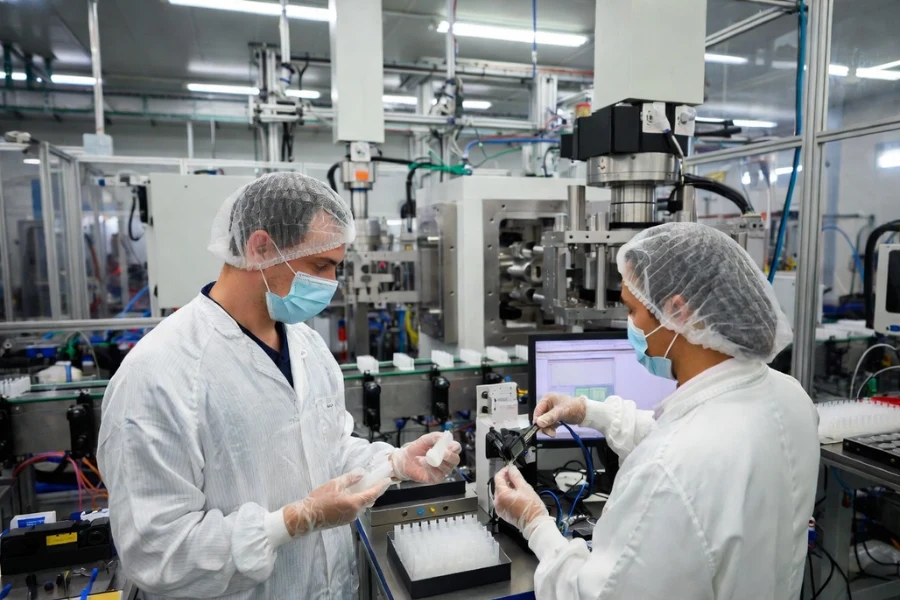
Medical applications may introduce additional requirements for resin selection, traceability, contamination control, dimensional consistency and process control. Depending on the product, medical plastic injection molding may also be performed in controlled environments such as cleanroom injection molding.
Automotive
Automotive applications include housings, clips, connectors, interior components and structural polymer parts. Material selection depends on factors such as mechanical load, temperature exposure, chemical resistance and appearance.
Food and Packaging
Caps, closures, containers and dispensing components are commonly injection molded. Materials and manufacturing conditions must meet the functional and applicable food-contact requirements of the product.
Consumer and Industrial Products
Appliances, electronics, tools, fittings, housings, fasteners and numerous household or industrial components are produced through injection molding. The process can combine functional features and assembly details in a repeatable molded part.
What Determines Injection Molding Cost?
Injection molding cost depends on tooling, material, machine requirements, cycle time, production volume and secondary operations.
| Cost Factor | Typical Impact |
|---|---|
| Tooling complexity | Cavities, slides, lifters, surface requirements and mold material affect upfront tooling cost |
| Material | Resin price, part weight and process yield influence material cost per part |
| Cycle time | Longer filling, packing or cooling increases machine time per component |
| Production volume | Higher quantities distribute tooling investment across more parts |
| Cavity count | More cavities can increase output per cycle but also increase tooling complexity |
| Secondary operations | Machining, printing, assembly, inspection and packaging add downstream cost |
Early injection mold design and manufacturability review can identify geometry that unnecessarily increases tooling or production complexity.
Higher cavity counts and more automation do not automatically create the lowest unit cost. The appropriate production strategy depends on expected volume, part geometry, quality requirements and the required manufacturing life of the program.
What Do Injection Molding Manufacturers Do?
Injection molding manufacturers vary in scope. Some primarily operate customer-supplied tooling, while integrated manufacturers may support development through finished-product operations.
Typical capabilities can include:
- Product and DFM review
- Prototyping
- Mold design
- Mold making
- Material evaluation
- Injection molding production
- Process development and quality control
- Secondary operations
- Assembly
- Packaging
For medical-device programs, manufacturing requirements can extend beyond molding itself to include material documentation, process controls, inspection, traceability, assembly and packaging.
SeaSkyMedical supports medical manufacturing programs across product development, tooling, injection molding and related downstream manufacturing operations.
Conclusion
Injection molding is most effective when material behavior, part design, tooling and process conditions are evaluated as one manufacturing system. Its production and cost advantages become strongest when part requirements and volume justify dedicated tooling.